3-Axis CNC Milling Services
Resolute Precision Manufacturing's 3-axis CNC milling services deliver precision prismatic parts in steel, aluminum, stainless, brass, and engineering plastics. Three-axis milling is the most efficient and cost-effective method for the majority of milled part requirements and with ISO 9001 certified quality controls and 24-hour quote response, it is also one of the fastest ways to get your parts into production. Request a QuoteWhat 3-Axis CNC Milling Produces
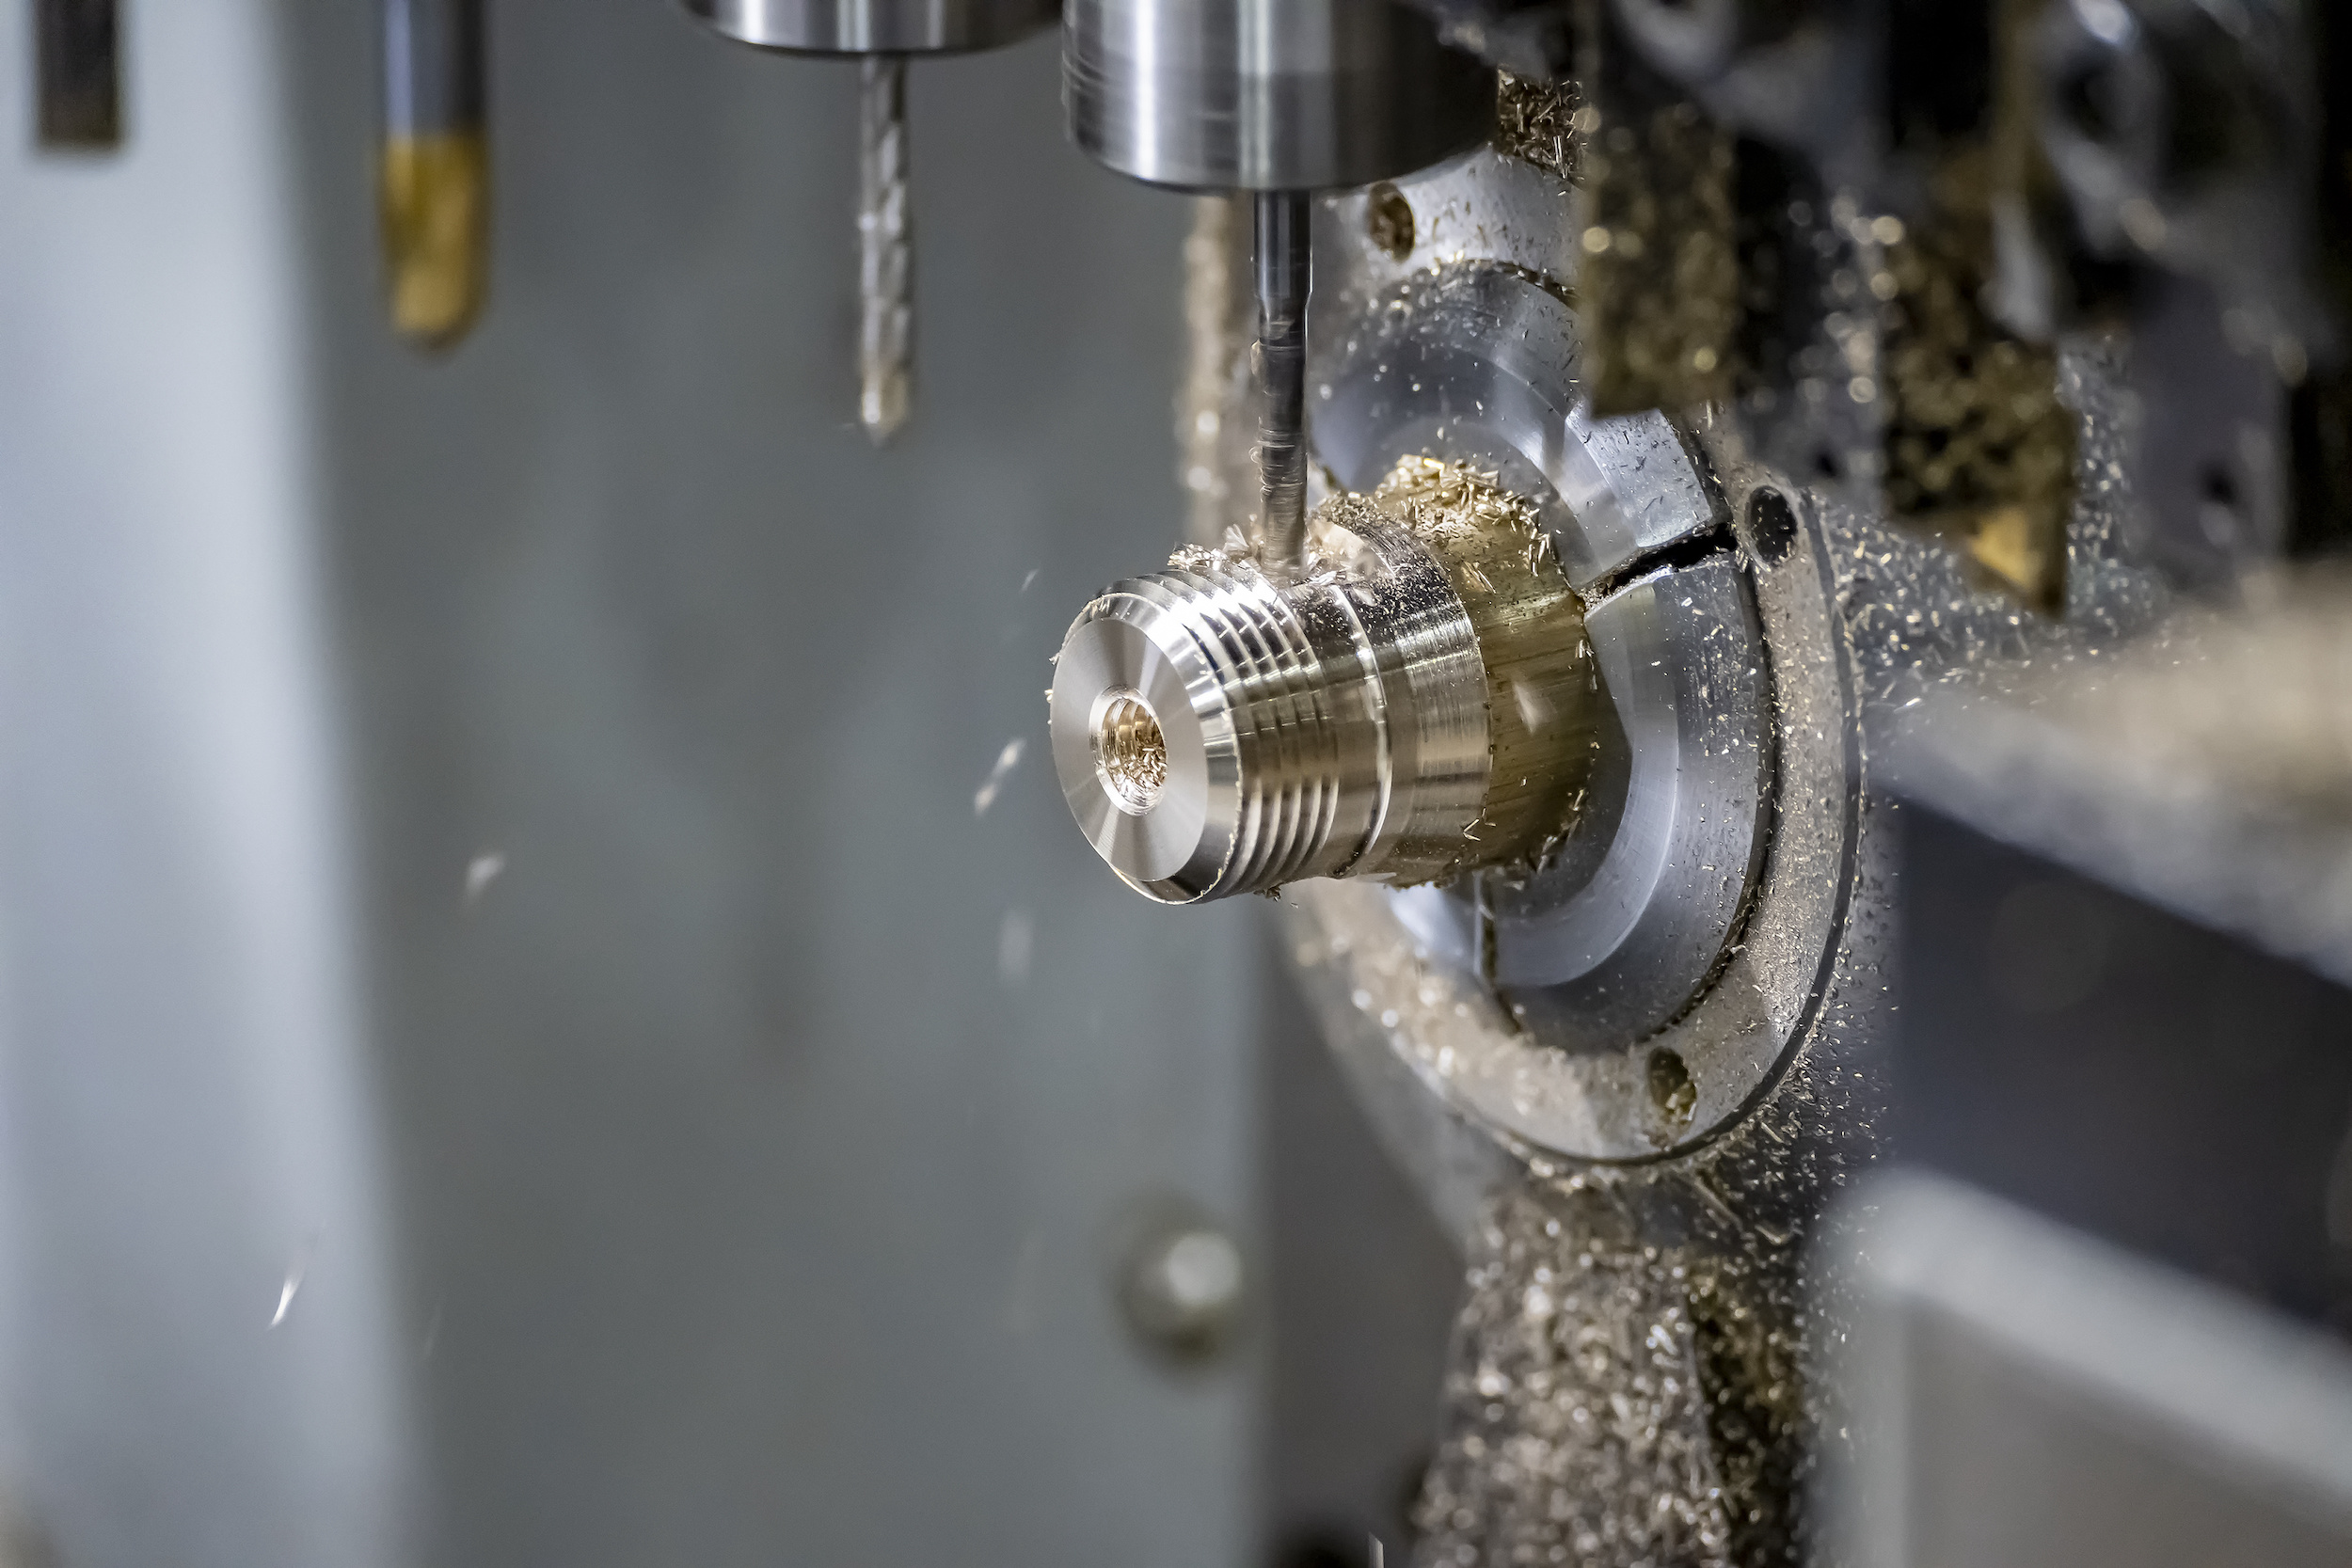
In 3-axis CNC milling, the cutting tool moves in three linear directions: X (left-right), Y (front-back), and Z (up-down). The workpiece is stationary on the table while the spindle executes the programmed cutting path. This configuration efficiently produces all standard prismatic features flat faces, rectangular pockets, profiled contours, drilled and tapped holes, counterbores, and chamfers.
Three-axis milling is the right choice for the majority of bracket, plate, housing, and fixture requirements. It is faster to set up, more widely applicable, and lower in cost than 4 or 5-axis machining for parts that do not require compound-angle or rotational features.
Our Services
When to Choose 3-Axis Over 4 or 5-Axis
Three-axis milling is the optimal choice when your part’s features can all be accessed from one or two setup orientations. For parts requiring features on one face, two parallel faces, or four orthogonal faces (with re-fixturing between setups), 3-axis milling is the most cost-effective approach. When features require angular orientation that cannot be achieved by re-fixturing, 4 or 5-axis machining becomes appropriate.
Specifications
| Axes | X, Y, and Z — three linear axes |
| Motion | Cutting tool moves in X, Y, and Z while the workpiece remains stationary on the table |
| Work Envelope | Up to 20″ × 50″ on our vertical machining centers |
| Operations | Face milling, pocket milling, profile milling, drilling, tapping, boring, counterboring, chamfering |
| Tooling | CAT40 — full range of roughing and finishing end mills, drills, taps, and boring bars |
| Tolerance | ±0.001″ standard; tighter tolerances available on request |
| Surface Finish | Ra 125 microinch standard; finer finishes available with appropriate tooling and process |
| Volume | 1 prototype to high-volume production |
| Certifications | ISO 9001:2015 |
Common 3-Axis Milled Part Types
Three-axis milling efficiently produces the following part families:
Brackets and mounting plates — flat stock with holes, slots, and profiled edges
Rectangular housings — pocketed enclosures with bosses, ports, and mounting features
Flanges — faced, drilled, and tapped flat components
Tooling plates — precision-dimensioned reference fixtures with array-drilled hole patterns
Manifold blanks — flat-faced blocks with drilled and tapped port patterns
Spacers and adapter plates — flat components with precision thickness and hole patterns
Frequently Asked Questions
Is 3-axis milling sufficient for most prismatic parts?
Yes. The majority of brackets, plates, housings, and fixtures can be produced entirely with 3-axis milling. Features on multiple faces are accommodated by re-fixturing the part between setups. We assess your drawing and recommend the most cost-effective machining approach.
What is the minimum feature size RPM can mill with a 3-axis machine?
Minimum feature size depends on the cutting tool diameter required. We routinely mill pockets and slots as narrow as 0.030″ with appropriate tooling. Contact us with your drawing for a feasibility assessment of fine features.
Can 3-axis milling achieve tight hole location tolerances?
Yes. With proper fixturing and tool path programming, 3-axis milling routinely achieves hole location tolerances of ±0.001″ or better relative to datum features. True position tolerances are held to drawing requirements using coordinate measuring machine (CMM) verification.
Does RPM offer 3-axis milling in prototype quantities?
Yes. We produce 3-axis milled prototypes from single pieces upward with 24-hour quote response and one to three week production lead time for most parts.