Custom Machined Shafts
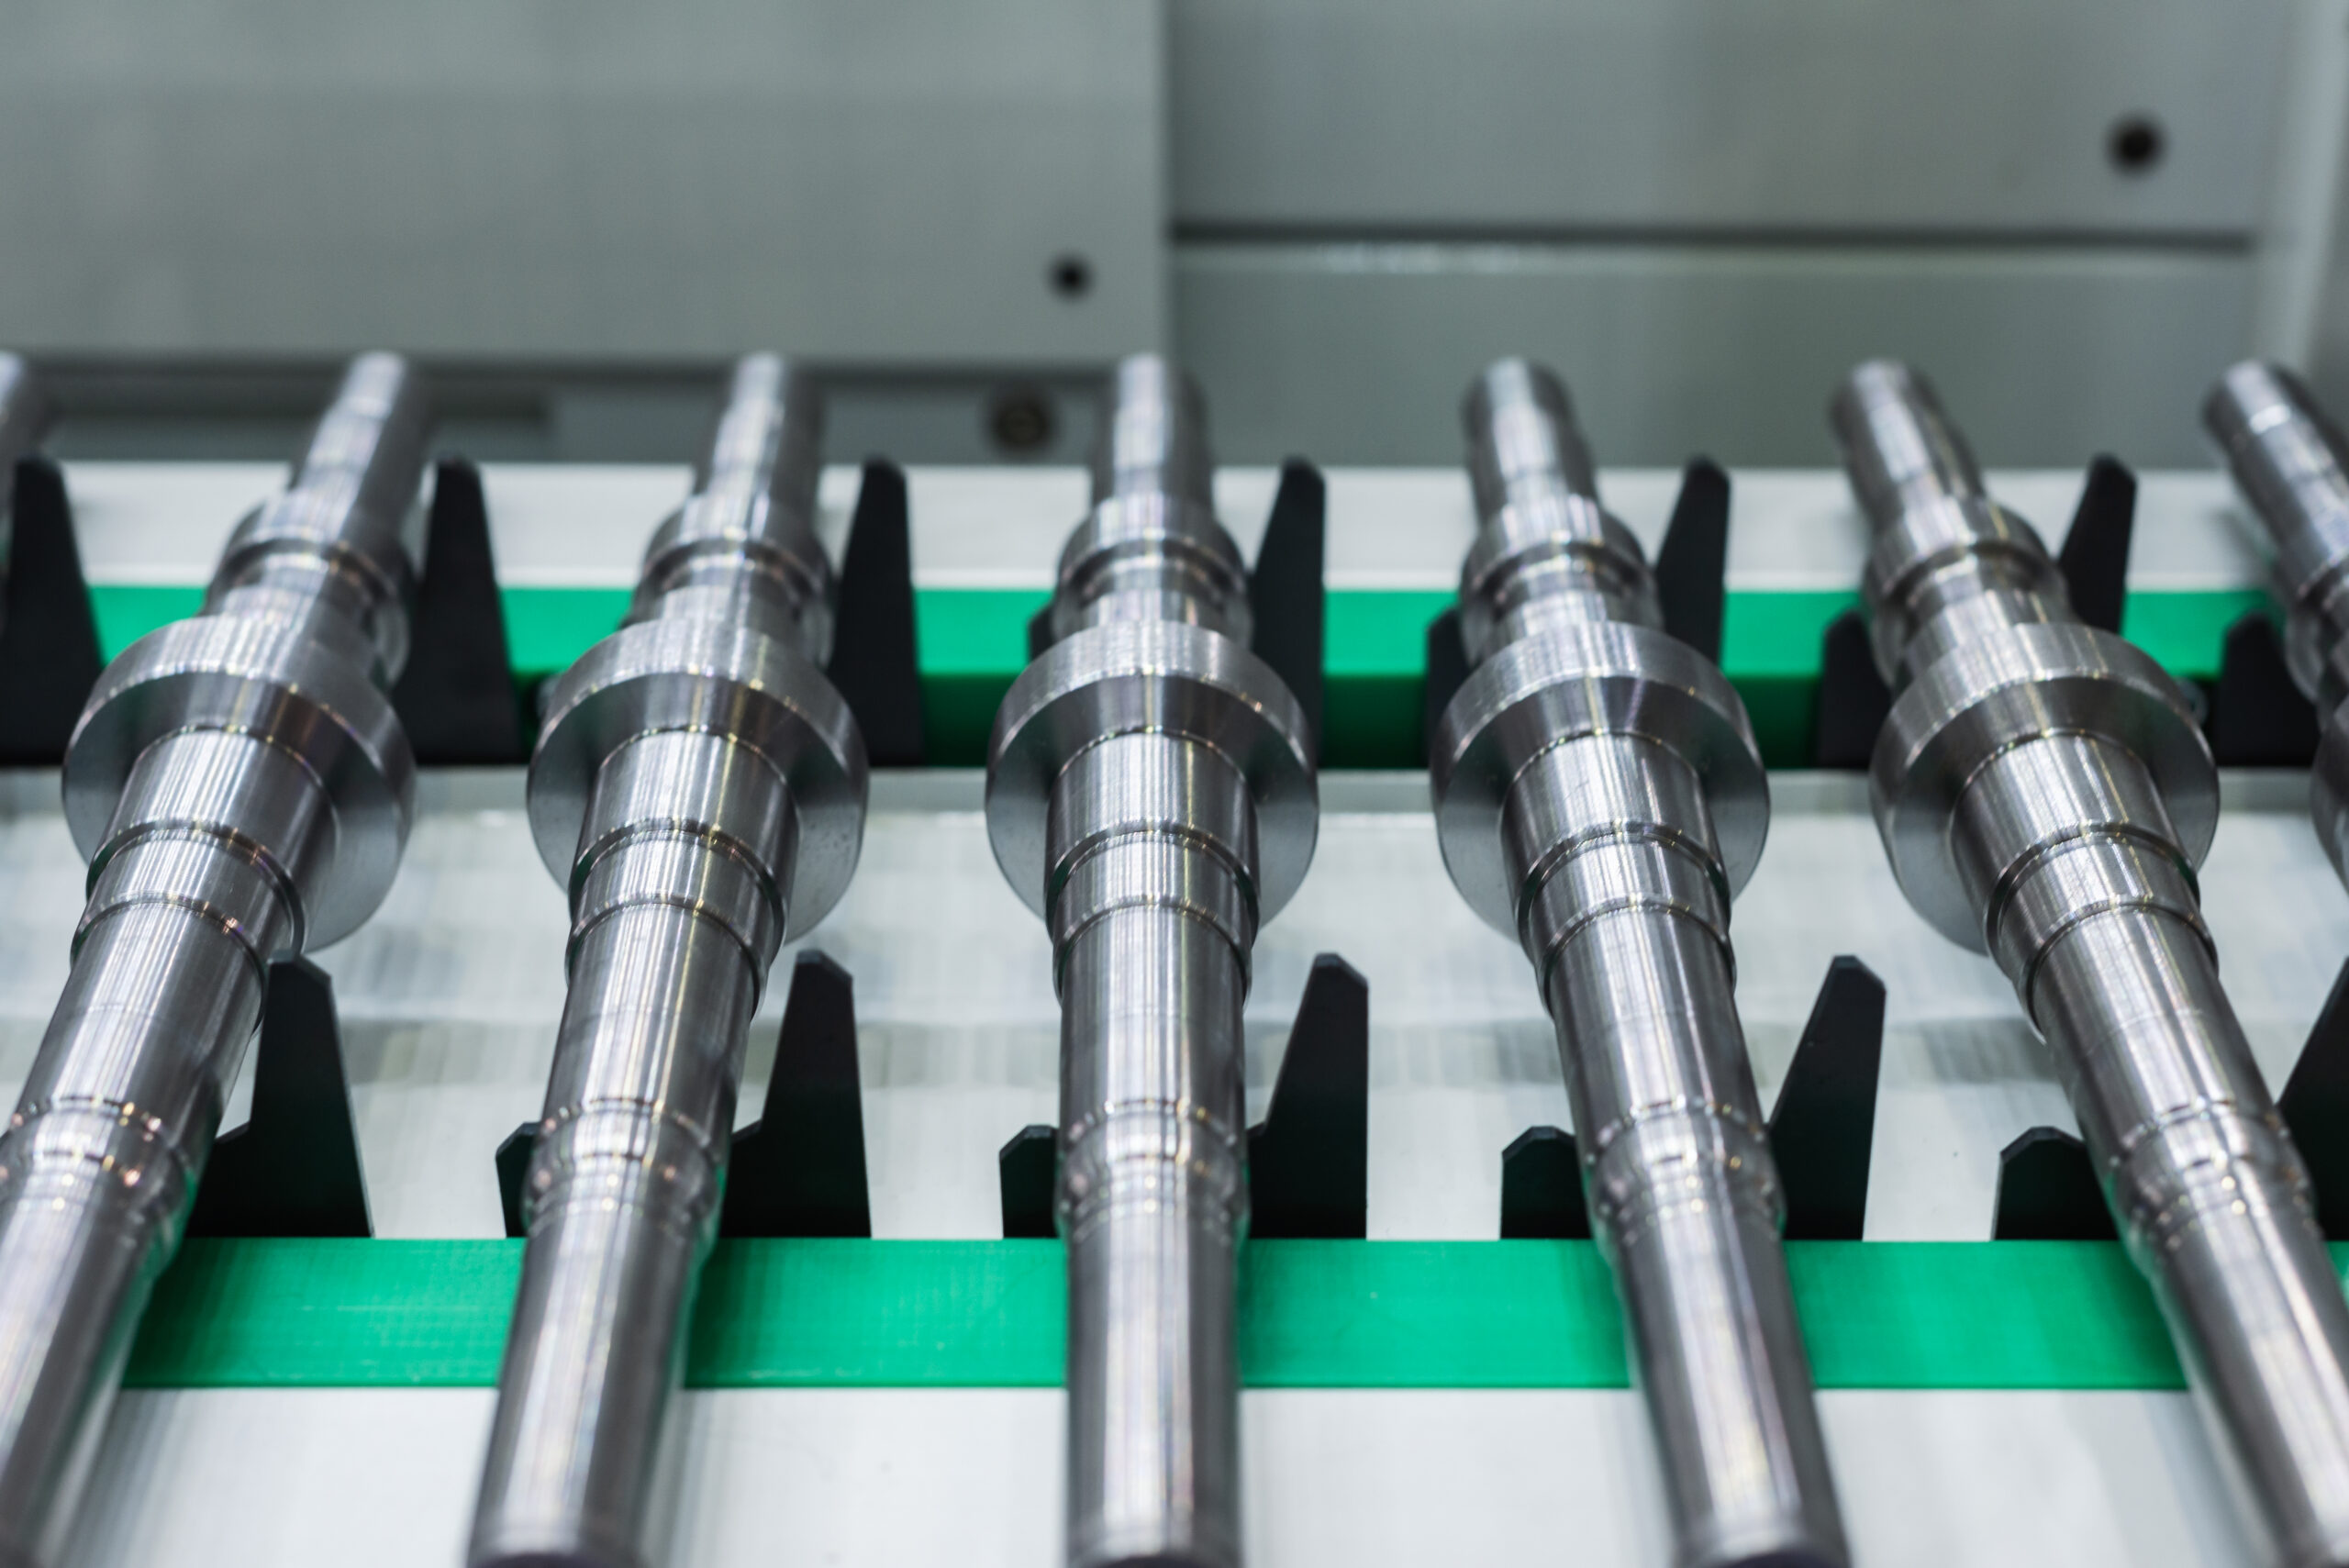
Resolute Precision Manufacturing produces precision CNC turned shafts to drawing — stepped shafts, splined shafts, keyed shafts, and threaded shafts — in steel, stainless, aluminum, and brass. From small diameter shafts on our Swiss CNC machines to large shafts up to 25.5 inches in diameter on our chucked turning centers, we produce shafts with all features complete in a single setup for maximum concentricity and accuracy. Request a QuoteShaft Geometry and the Case for Single-Setup Turning
Our Services
Shaft Features Machined in One Setup
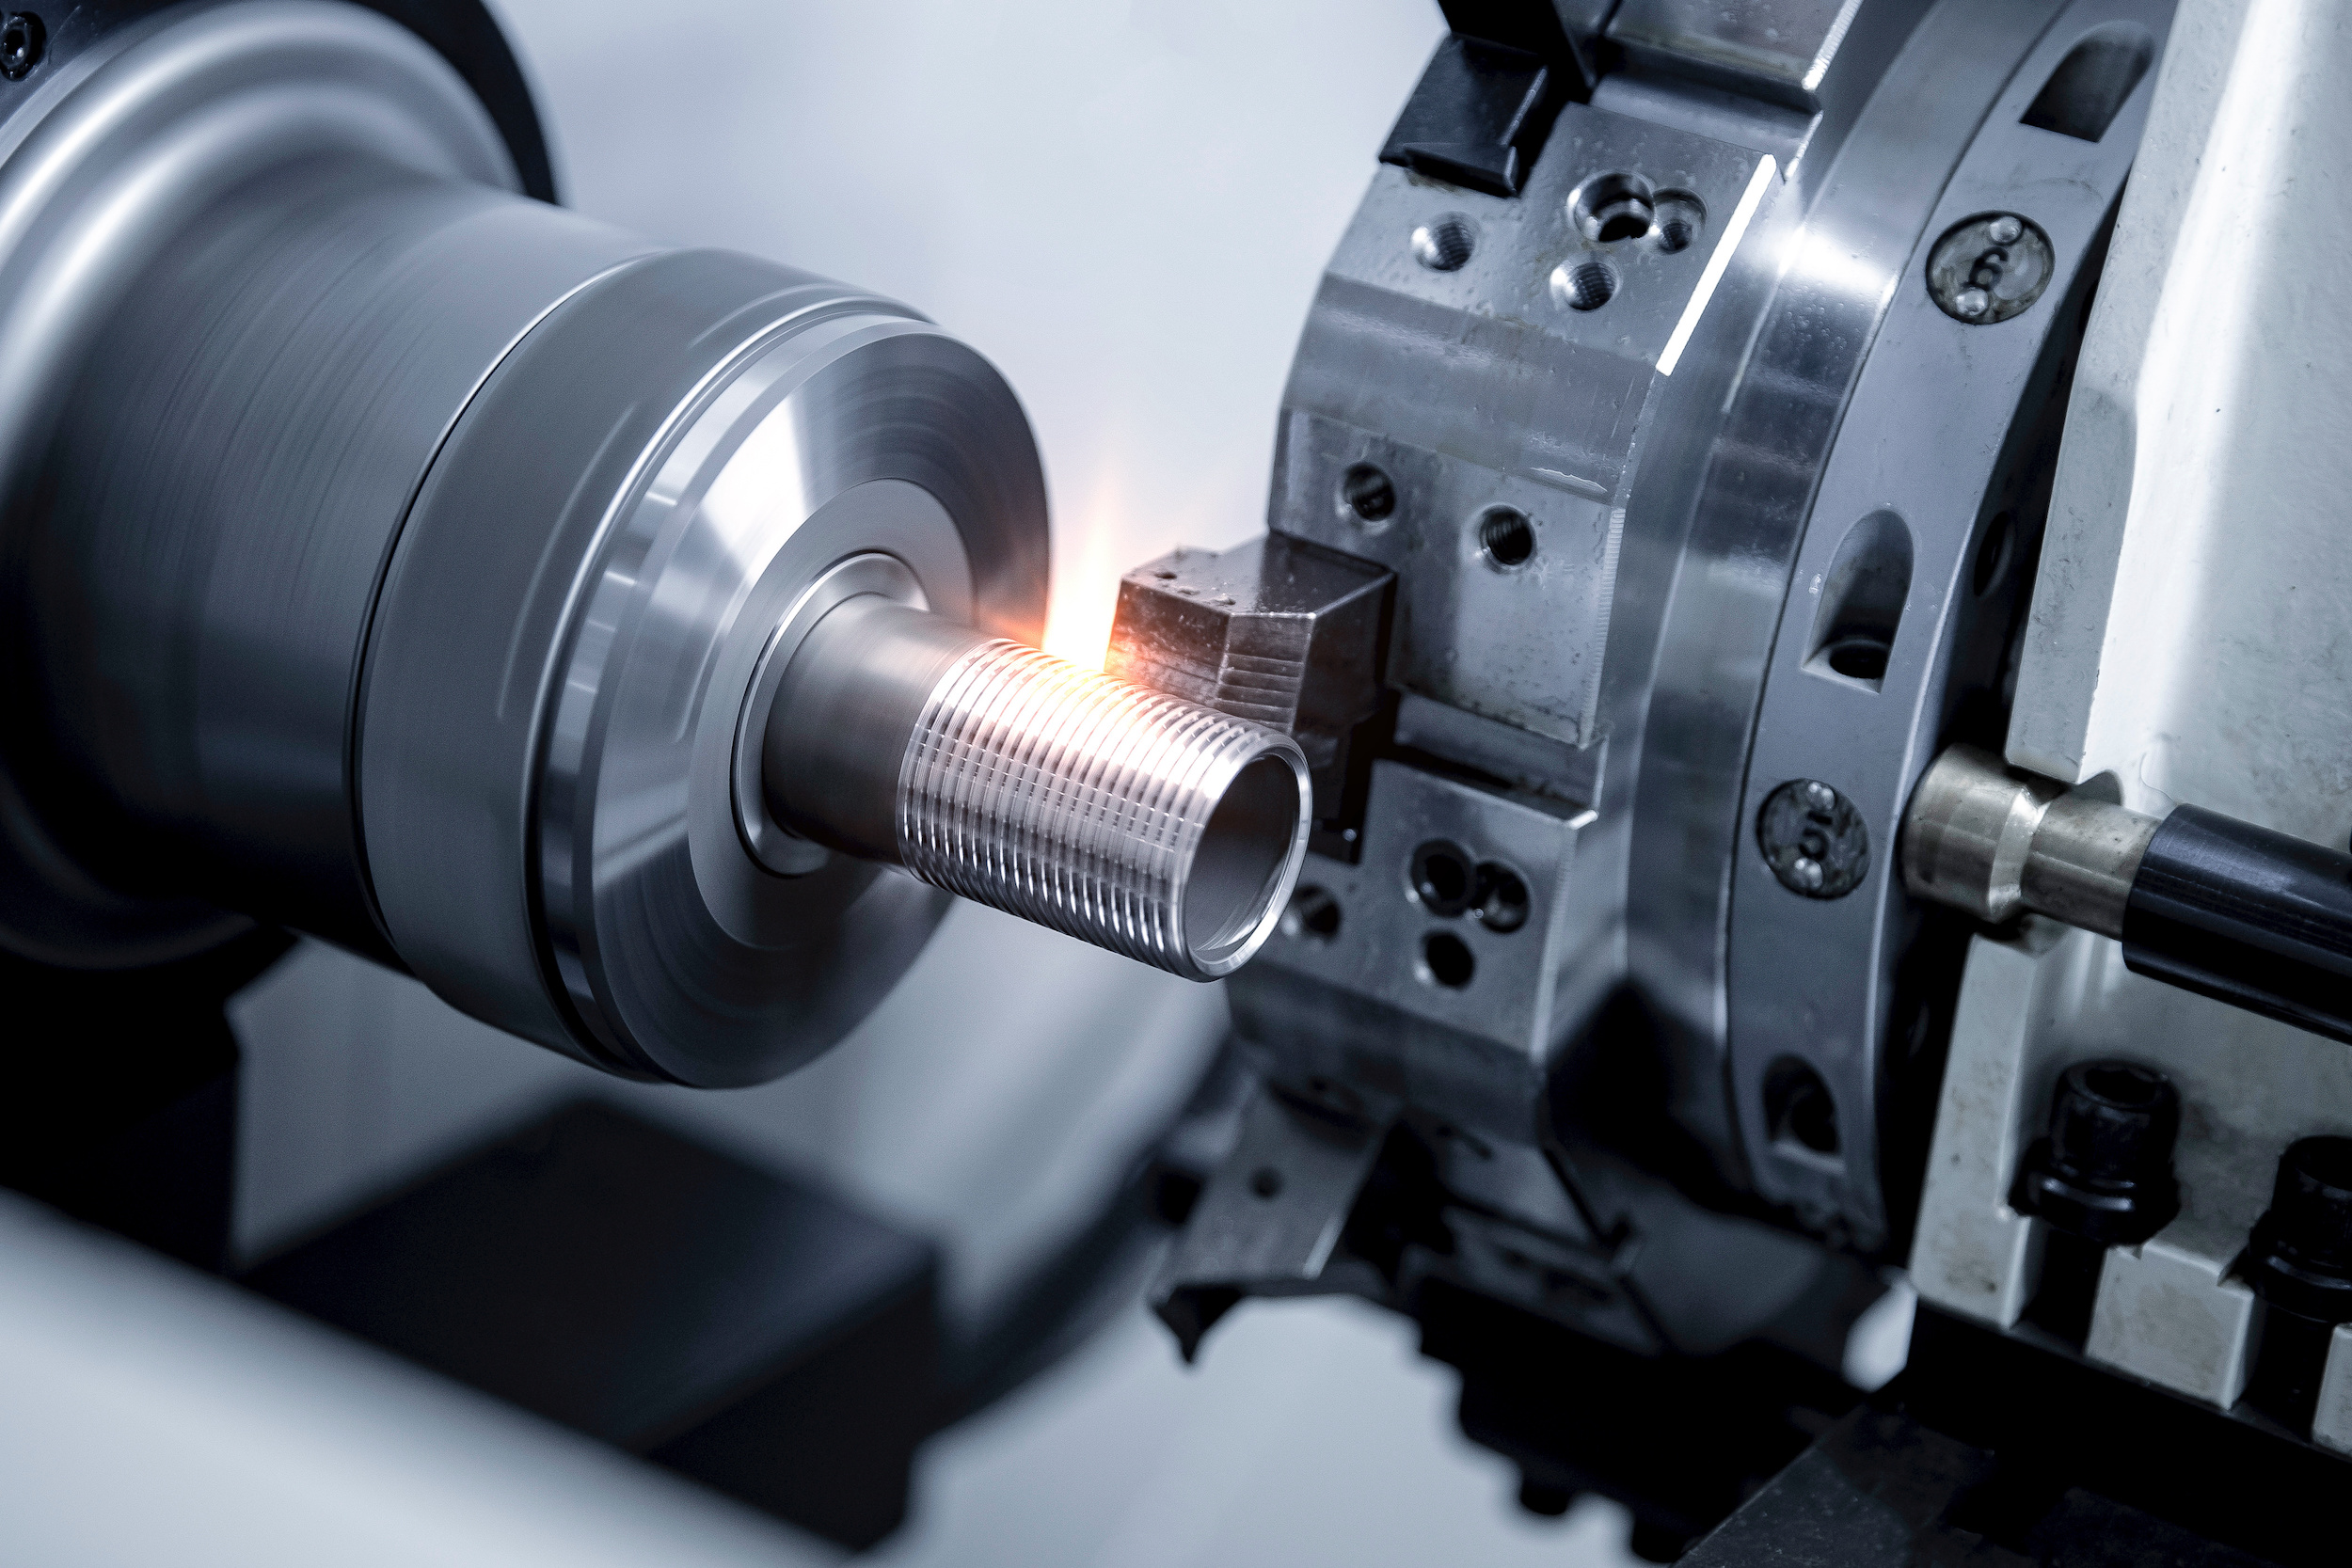
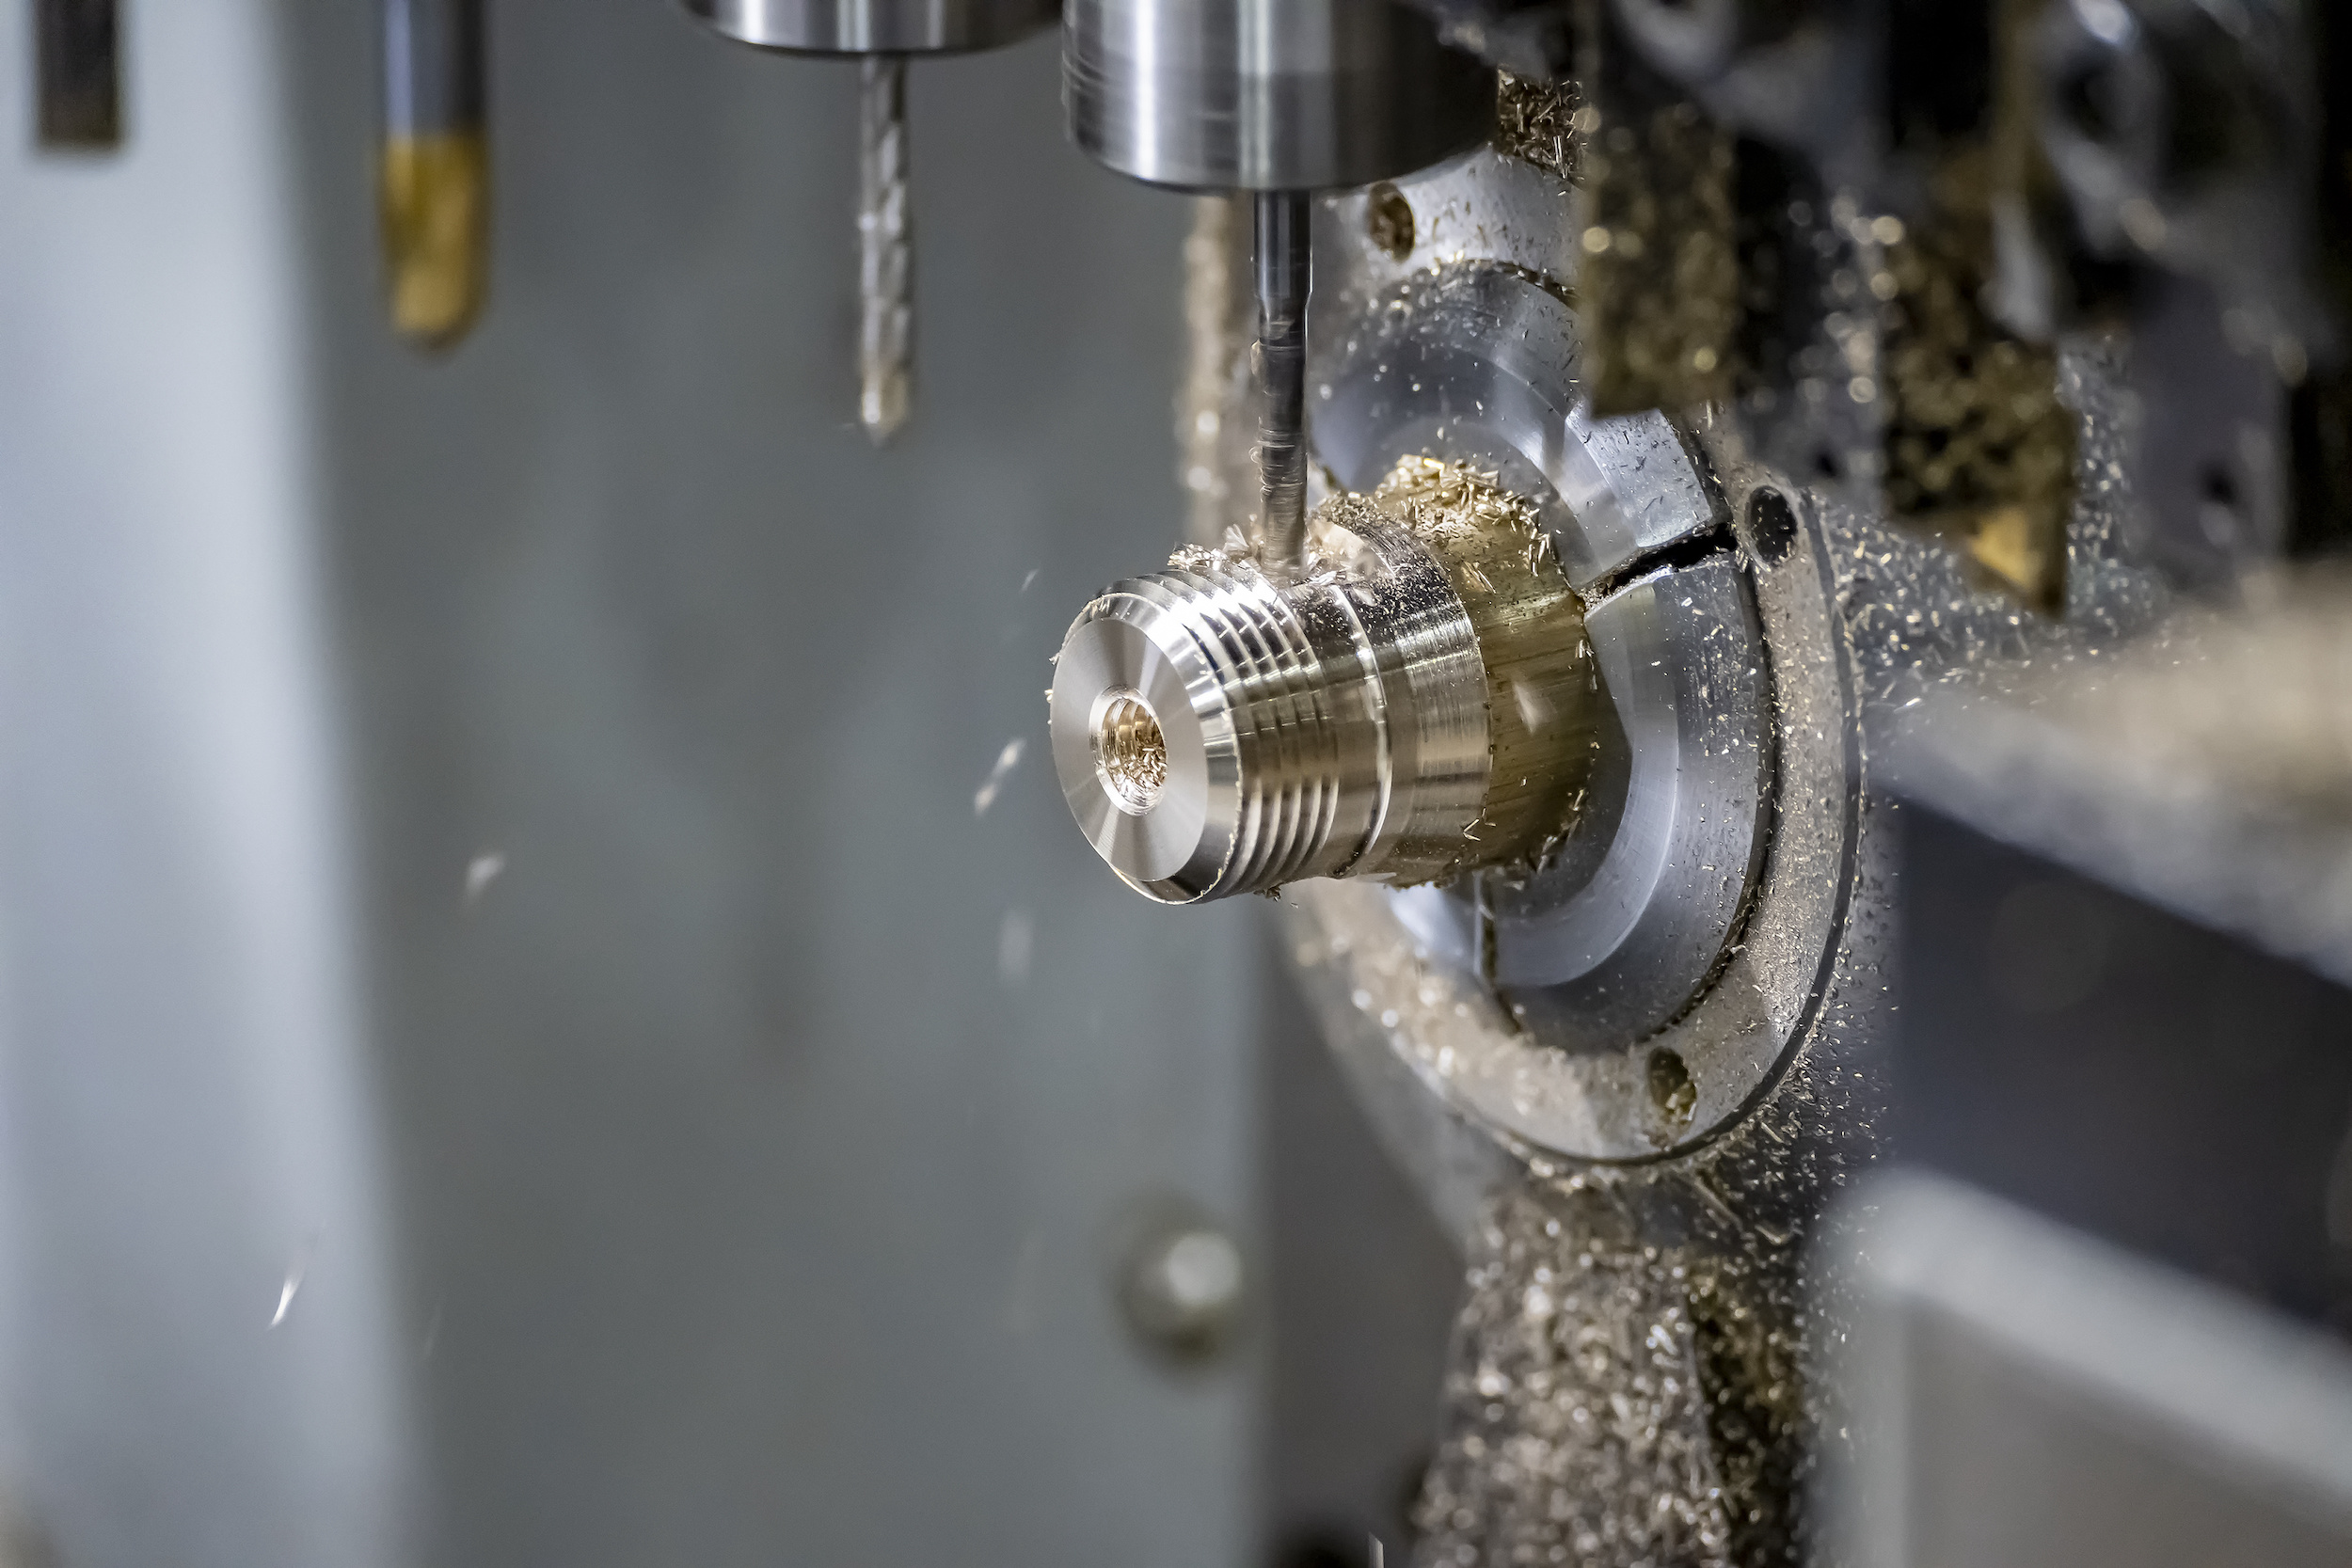
Our live tooling lathes complete all of the following shaft features without secondary operations:
- Stepped diameter profiles — Multiple OD steps turned and finished in sequence.
- Keyways — Milled with live tooling at any angular position along the shaft OD.
- Threaded ends — Internal and external threads at shaft ends completed in the same turning cycle.
- Flats and hex profiles — Live tooling mills drive flats at specified positions.
- Cross-holes and radial holes — Drilled with live tooling at any position and angle.
- Ground surfaces — Final OD grinding coordinated through outside operations for the highest surface finish.
Specifications
| Diameter Range | Small shafts on Swiss CNC (up to 38mm); standard shafts bar-fed up to 3.2″; large shafts chucked up to 25.5″ |
| Length | Bar-fed: up to 12′ long; chucked: up to 44″ length |
| Keyways | Milled with live tooling in the same setup; parallel, Woodruff, and custom profiles |
| Threads | Internal and external threads at shaft ends; any thread form and pitch |
| Runout | Concentric turning in one setup; bearing seat runout up to 0.0005″ TIR achievable |
| Surface Finish | As-machined Ra 32–63 microinch standard; ground finish coordinated for Ra 16 or better |
| Metals | Steel (1018/4140/4340/8620), stainless steel (303/304/316/17-4PH), aluminum (6061/7075), brass |
| Heat Treatment | Coordinated through outside operations; quench & temper (Q&T), induction hardening, and carburizing available |
| Certifications | ISO 9001:2015 |
Shaft Applications From RPM
- Motor and gearbox shafts — Stepped OD shafts with keyways and bearing seat diameters.
- Pump shafts — Sealed-surface shafts in stainless steel for fluid handling applications.
- Conveyor drive shafts — Alloy steel shafts with spline or key drive features.
- Medical device shafts — Small-diameter stainless steel shafts for surgical instrument drives.
- Aerospace actuator shafts — Titanium and 17-4 PH stainless steel shafts for flight control systems.
- Precision spindle shafts — High-accuracy shafts for machine tool and metrology applications.
Frequently Asked Questions
What is the straightness tolerance RPM can hold on a long shaft?
Straightness on long shafts is influenced by material residual stress, work holding, and turning parameters. For shafts requiring tight straightness, we use steady rests and controlled cutting parameters. Typical straightness of 0.001″ per foot is achievable on properly supported shafts in stress-relieved material.
Can RPM produce splined shafts ?
Yes. Involute splines and parallel key splines are machined on our mill/turn and live tooling lathes. For standard ANSI or DIN spline profiles, we machine to the standard specification. Custom spline profiles are machined to drawing.
What material is recommended for a shaft requiring both strength and corrosion resistance?
17-4 PH stainless steel is the most common choice — it offers high tensile strength (up to 220 KSI condition H900) combined with good corrosion resistance. For less demanding corrosion environments, 4140 steel with appropriate coating provides a lower-cost alternative.
Can RPM coordinate grinding to a final shaft diameter after turning?
Yes. Through our outside operations services, we coordinate OD grinding to specified diameter and surface finish after turning and heat treatment. We manage the complete process — you receive a fully finished shaft from one purchase order.