4-Axis CNC Milling Services
Resolute Precision Manufacturing's 4-axis CNC milling adds a rotational A or B axis to standard 3-axis milling enabling the machining of features at multiple angular positions around a cylindrical or prismatic workpiece in a single setup. Reduce setups, improve accuracy, and shorten lead time on parts that would otherwise require multiple re-fixturings on a 3-axis machine. Request a QuoteWhat the 4th Axis Adds
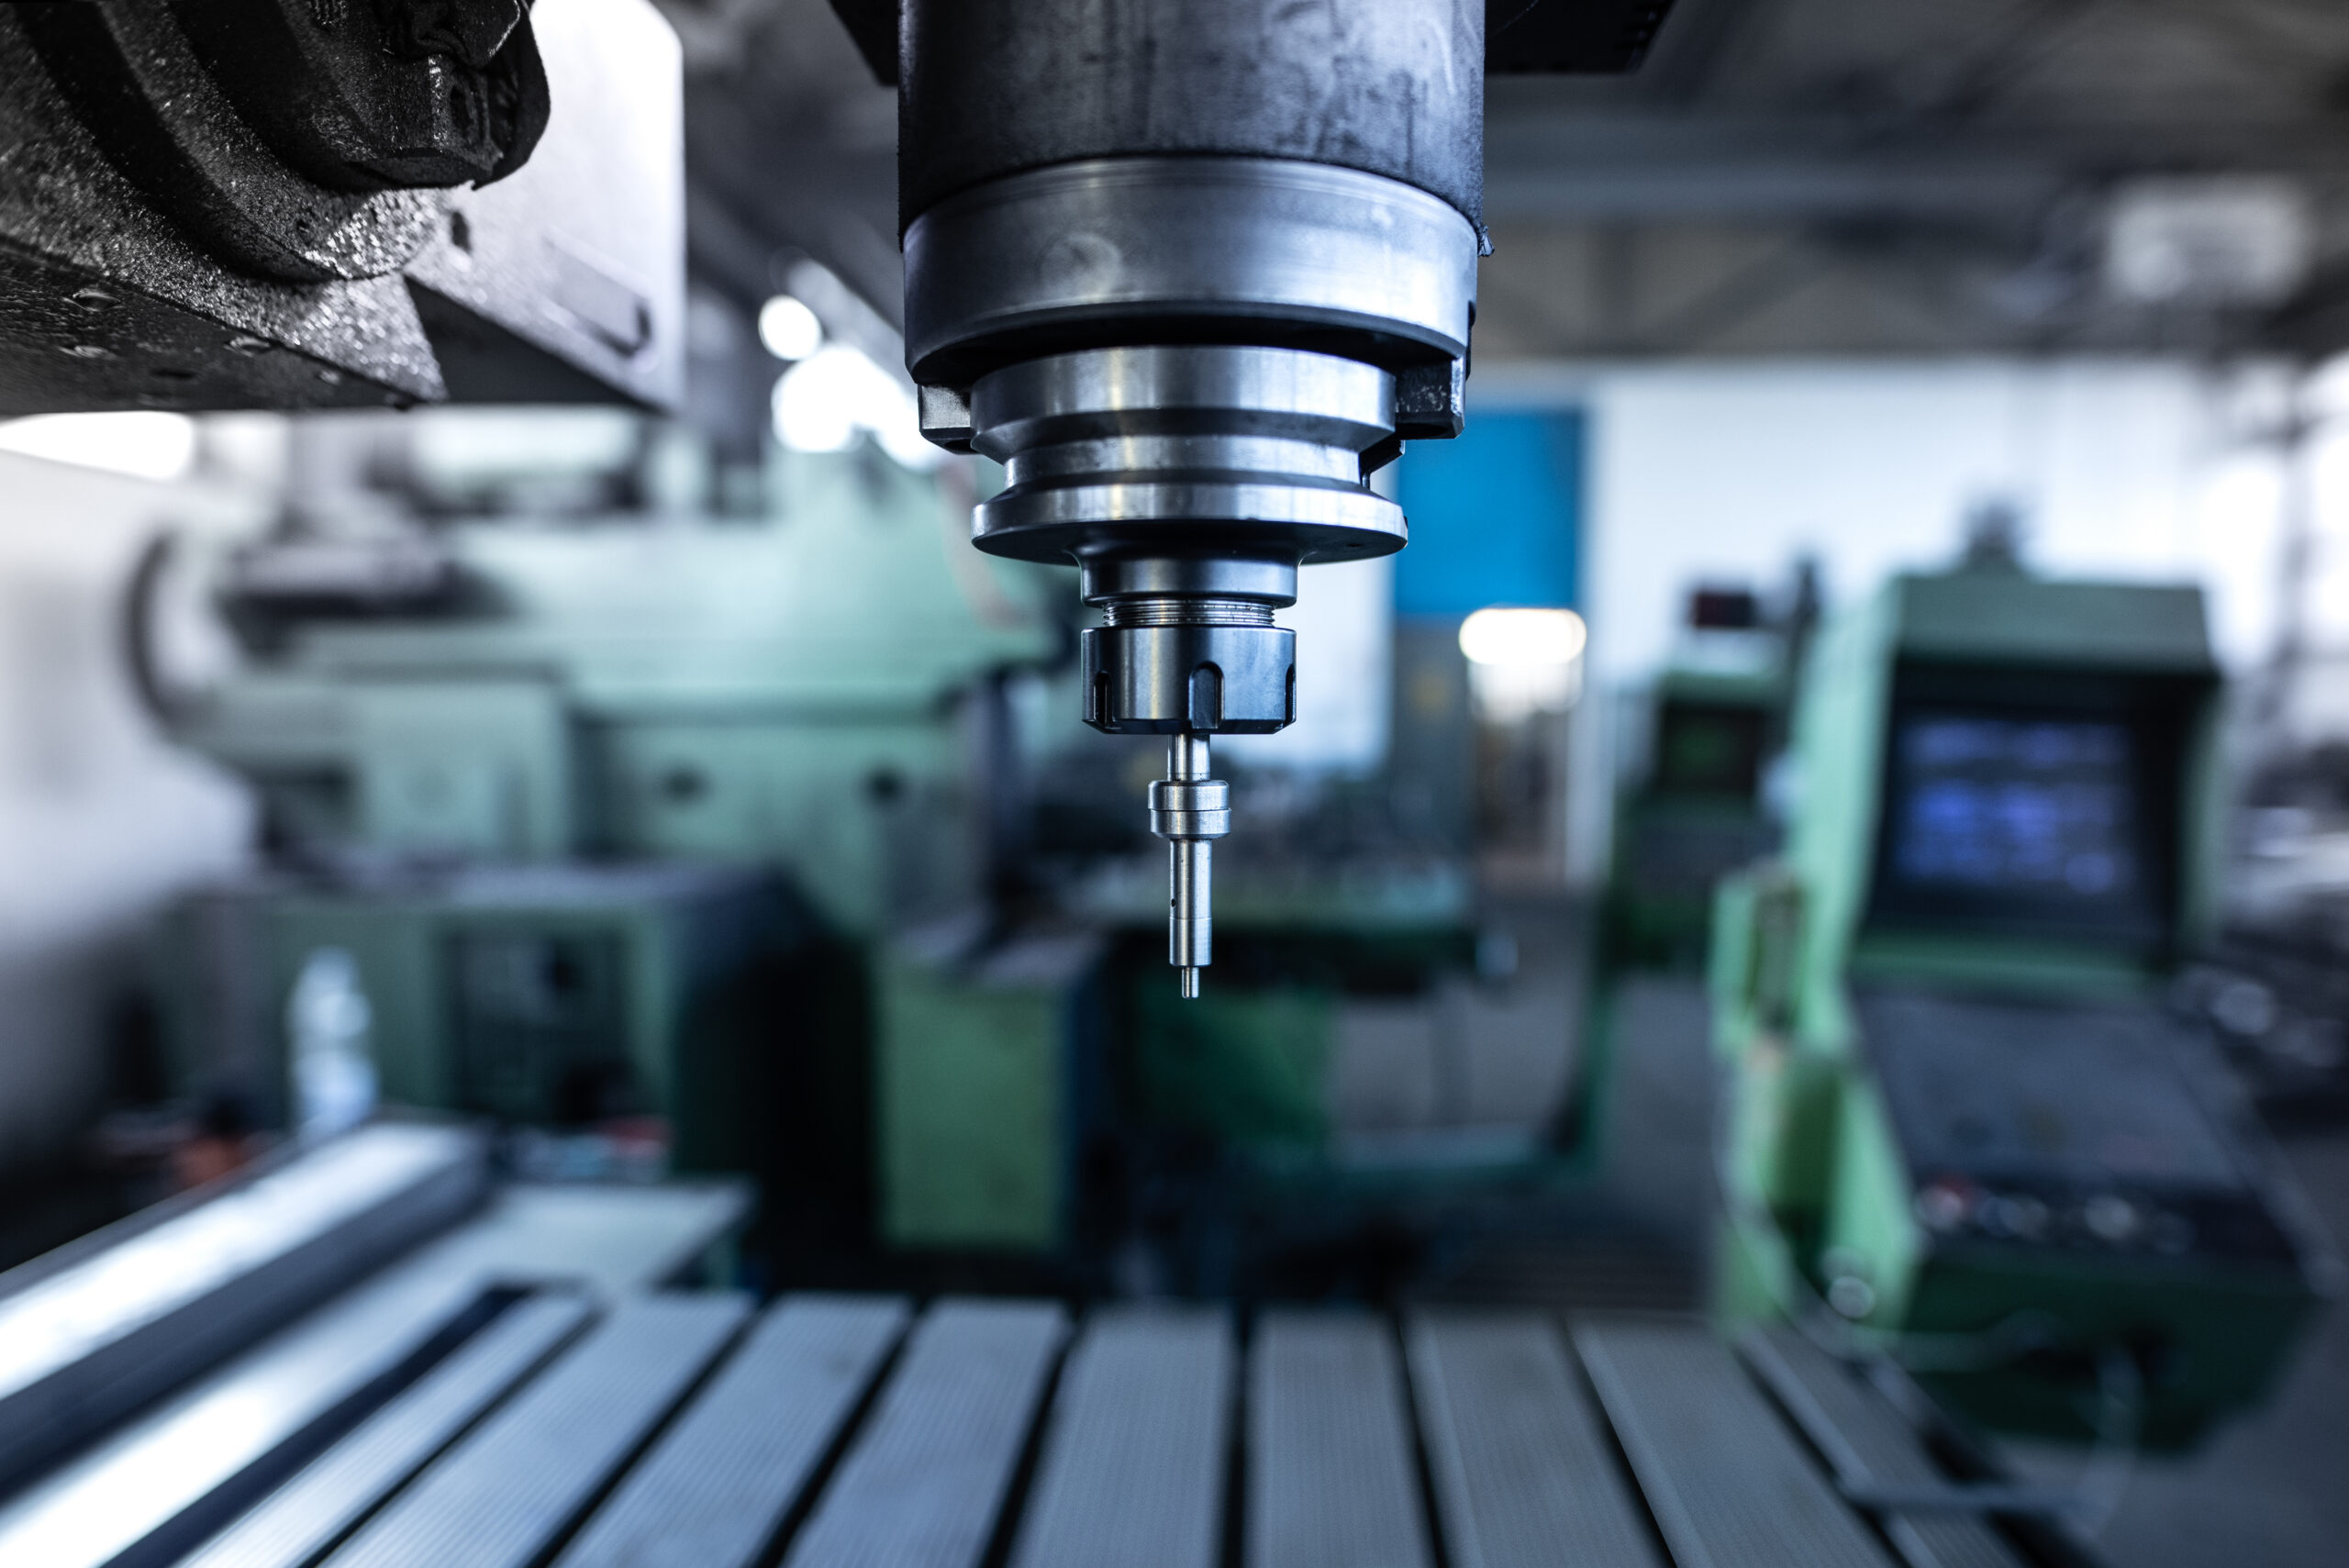
In 4-axis CNC milling, a rotary table or indexing head holds the workpiece and rotates it around one additional axis typically the A-axis (rotation about X) or the B-axis (rotation about Y). The machine can index the part to any angular position and then perform standard 3-axis milling at that position. This is sometimes called 3+1 machining, as the fourth axis is used for positioning rather than simultaneous cutting motion.
The practical benefit is the ability to machine features on multiple faces of a part flats, holes, slots, pockets without removing and re-fixturing the part between operations. Each re-fixturing on a 3-axis machine introduces a small re-referencing error that accumulates across features. The 4-axis approach maintains a single datum throughout all faces, improving positional accuracy between features.
Our Services
Indexed vs. Simultaneous 4-Axis
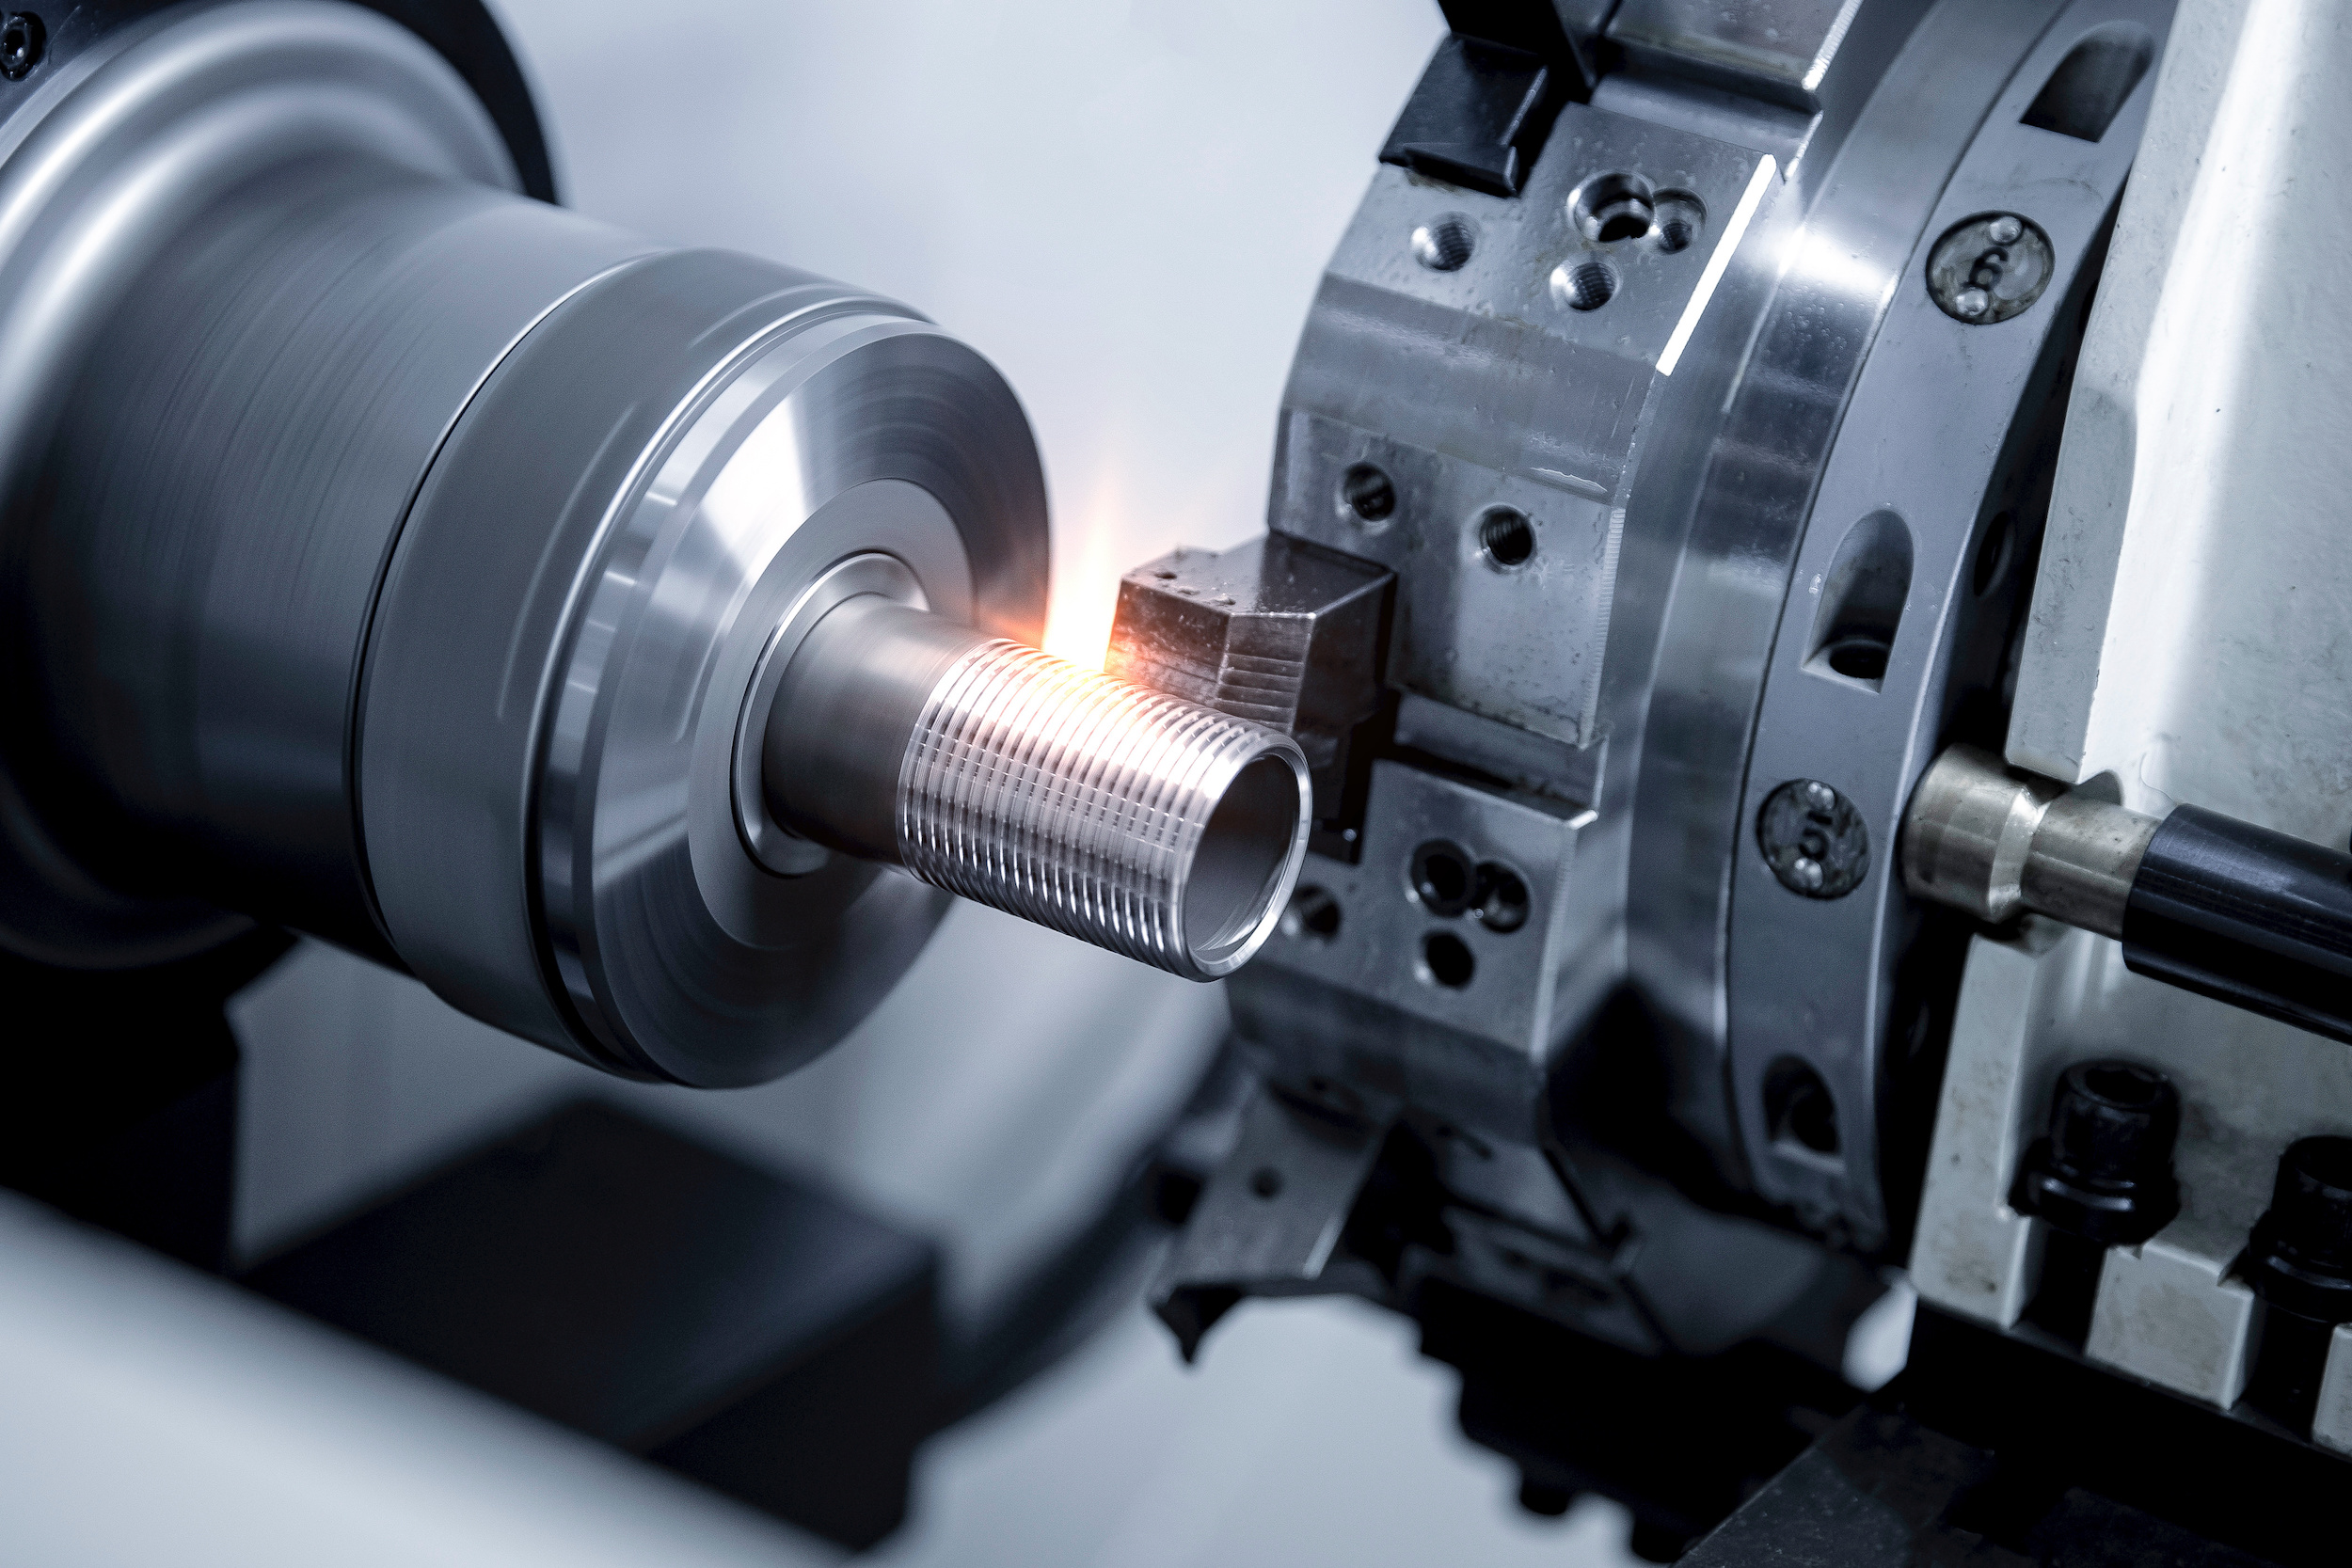
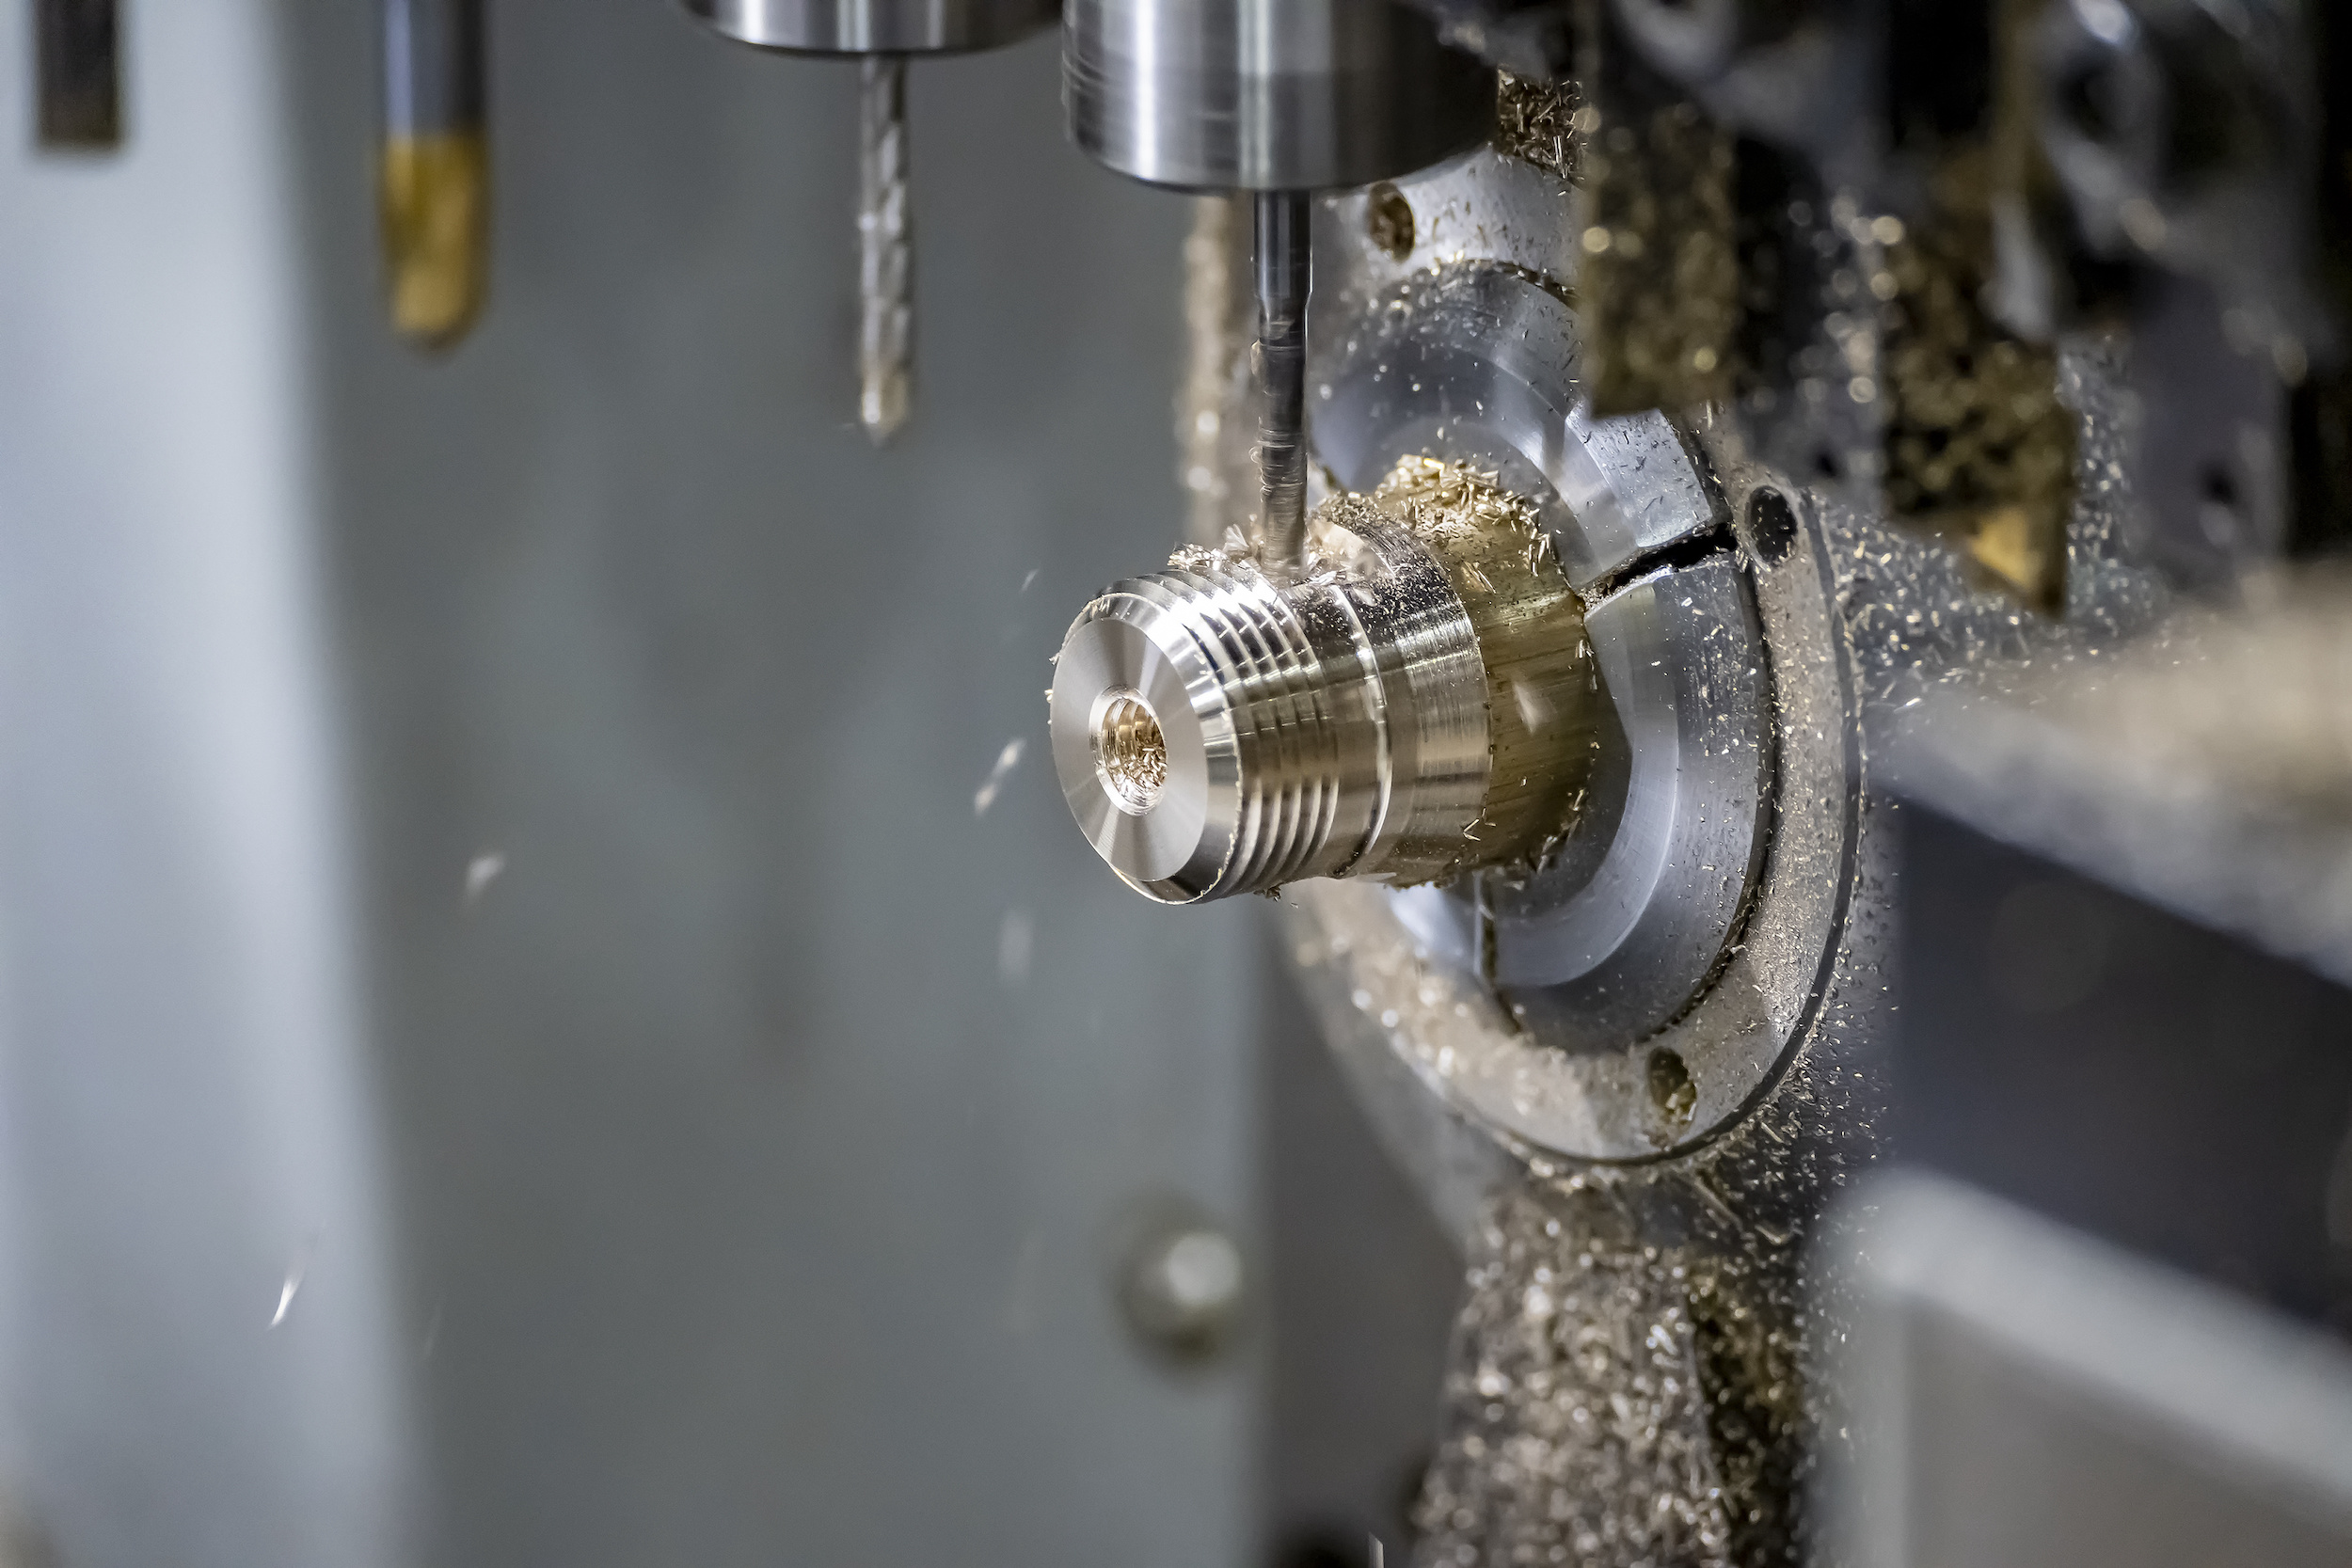
Four-axis machining can be performed in two modes. In indexed mode, the rotary axis positions the part to a fixed angle, locks, and the machine mills with the standard three axes. In continuous mode, the rotary axis moves simultaneously with the three linear axes during cutting. Indexed 4-axis is used for features at defined angular positions. Continuous 4-axis is used for helical features, spiral paths, and cam profiles that require the part to rotate during cutting.
Specifications
| Axes | X, Y, and Z — three linear axes |
| 4th Axis Mode | Indexed positioning or continuous simultaneous rotation during cutting |
| Angular Positioning | 0.001° resolution; any angular position around the rotational axis |
| Work Envelope | Up to 20″ × 50″ vertical machining center table; rotary table capacity depends on part size and weight |
| Tooling | CAT40 — full range of roughing and finishing tools |
| Tolerance | ±0.001″ standard; tighter tolerances available on request |
| Operations | All standard 3-axis operations plus features at any angular position |
| Materials | All standard metals and engineering plastics |
| Certifications | ISO 9001:2015 |
Parts Best Suited for 4-Axis Milling
Four-axis milling delivers the greatest advantage for these part families:
Cylindrical parts with milled flats, slots, keyways, or cross-holes at defined angular positions
Housings requiring milled features on four orthogonal faces without re-fixturing
Cam and eccentric profiles requiring continuous rotational motion during cutting
Parts with indexed hole patterns around a circular arc or bolt circle
Aerospace structural components requiring features on angled faces without fixturing complexity
Industrial machinery components with features at multiple rotational positions
Frequently Asked Questions
What is the difference between 4-axis and 5-axis milling?
Four-axis milling adds one rotational axis to the three linear axes, enabling features at any angular position around one axis. Five-axis adds a second rotational axis, enabling compound angles — features that require simultaneous tilt and rotation. If your part’s features can be described by rotation about a single axis, 4-axis is appropriate and more economical than 5-axis.
Can 4-axis milling replace separate setups on a 3-axis machine?
Yes this is the primary purpose of 4-axis machining. Parts requiring features on two, three, or four faces of a prismatic workpiece can often be completed in one 4-axis setup rather than multiple 3-axis setups. This improves accuracy and reduces lead time
What is the accuracy advantage of 4-axis over multiple 3-axis setups?
Each 3-axis re-setup introduces re-referencing error typically 0.001″ to 0.003″. A part requiring four 3-axis setups accumulates up to 0.012″ of potential positional error between features. Four-axis machining with a single datum eliminates this accumulation.
Does RPM offer 4-axis milling for prototype quantities?
Yes. We produce 4-axis milled prototypes from single pieces upward. The same machines and setups used for prototypes scale directly to production.