Nitride Service
Resolute Precision Manufacturing (RPM) offers nitride services for precision machined components that need hard, wear-resistant surfaces with minimal dimensional distortion. We coordinate ion nitriding and gas nitriding through our qualified outside processors. Unlike quench hardening, nitriding happens at relatively low temperatures and needs no quench, so distortion is far lower than with conventional heat treatment. We manage the complete process and deliver certified nitrided parts from a single purchase order. Request a QuoteWhat Nitriding Achieves
Nitriding is a thermochemical surface hardening process that diffuses nitrogen into the surface of steel parts, forming a hard compound layer and a diffusion zone below the surface. The compound layer (often called the white layer) provides exceptional wear resistance and moderate corrosion resistance. The diffusion zone gives a graduated transition between the hard surface and the core, which improves fatigue strength.
Because nitriding takes place below the lower critical temperature of steel, typically between 480°C and 565°C, the core properties set by prior heat treatment are not significantly altered, and no phase transformation or quench is needed. The result is a very hard surface with minimal distortion of the overall part geometry.
Ion Nitride vs. Gas Nitride
Two nitriding processes are available, chosen by part geometry, material, and surface requirement:
- Ion nitride (plasma nitride): nitrogen ions bombard the part surface in a vacuum chamber. It offers precise control of compound layer thickness, suits blind holes and complex geometry, and can minimize or eliminate the white layer per specification.
- Gas nitride: parts are exposed to an ammonia gas atmosphere in a furnace. The process has lower capital cost and longer cycle times, and white layer thickness is less controllable than with ion nitride. It suits large batches of simpler geometry.
Gas Nitriding Services Suppliers: Why Work With RPM
If you are comparing gas nitriding services suppliers, the questions that matter are who controls the process, who is accountable for dimensions, and how parts are documented. RPM is a machining company first. We machine your part, plan stock and finishing around the nitriding cycle, send it to a qualified processor, and inspect it in return. As one of the gas nitriding services suppliers you can order from together with machining, we remove a handoff between vendors and keep one team responsible for the finished part.
Nitride Services From Machining to Finished Part
Our nitride services follow a simple sequence:
- Machine and heat treat the part to the core condition you need (for example, quench and temper 4140 or 4340 before nitriding).
- Finish machine with allowance for the thin nitrided case, and grind or lap as required.
- Nitride by ion or gas process through a qualified processor.
- Inspect and document with hardness traverse, case depth, and white layer reports.
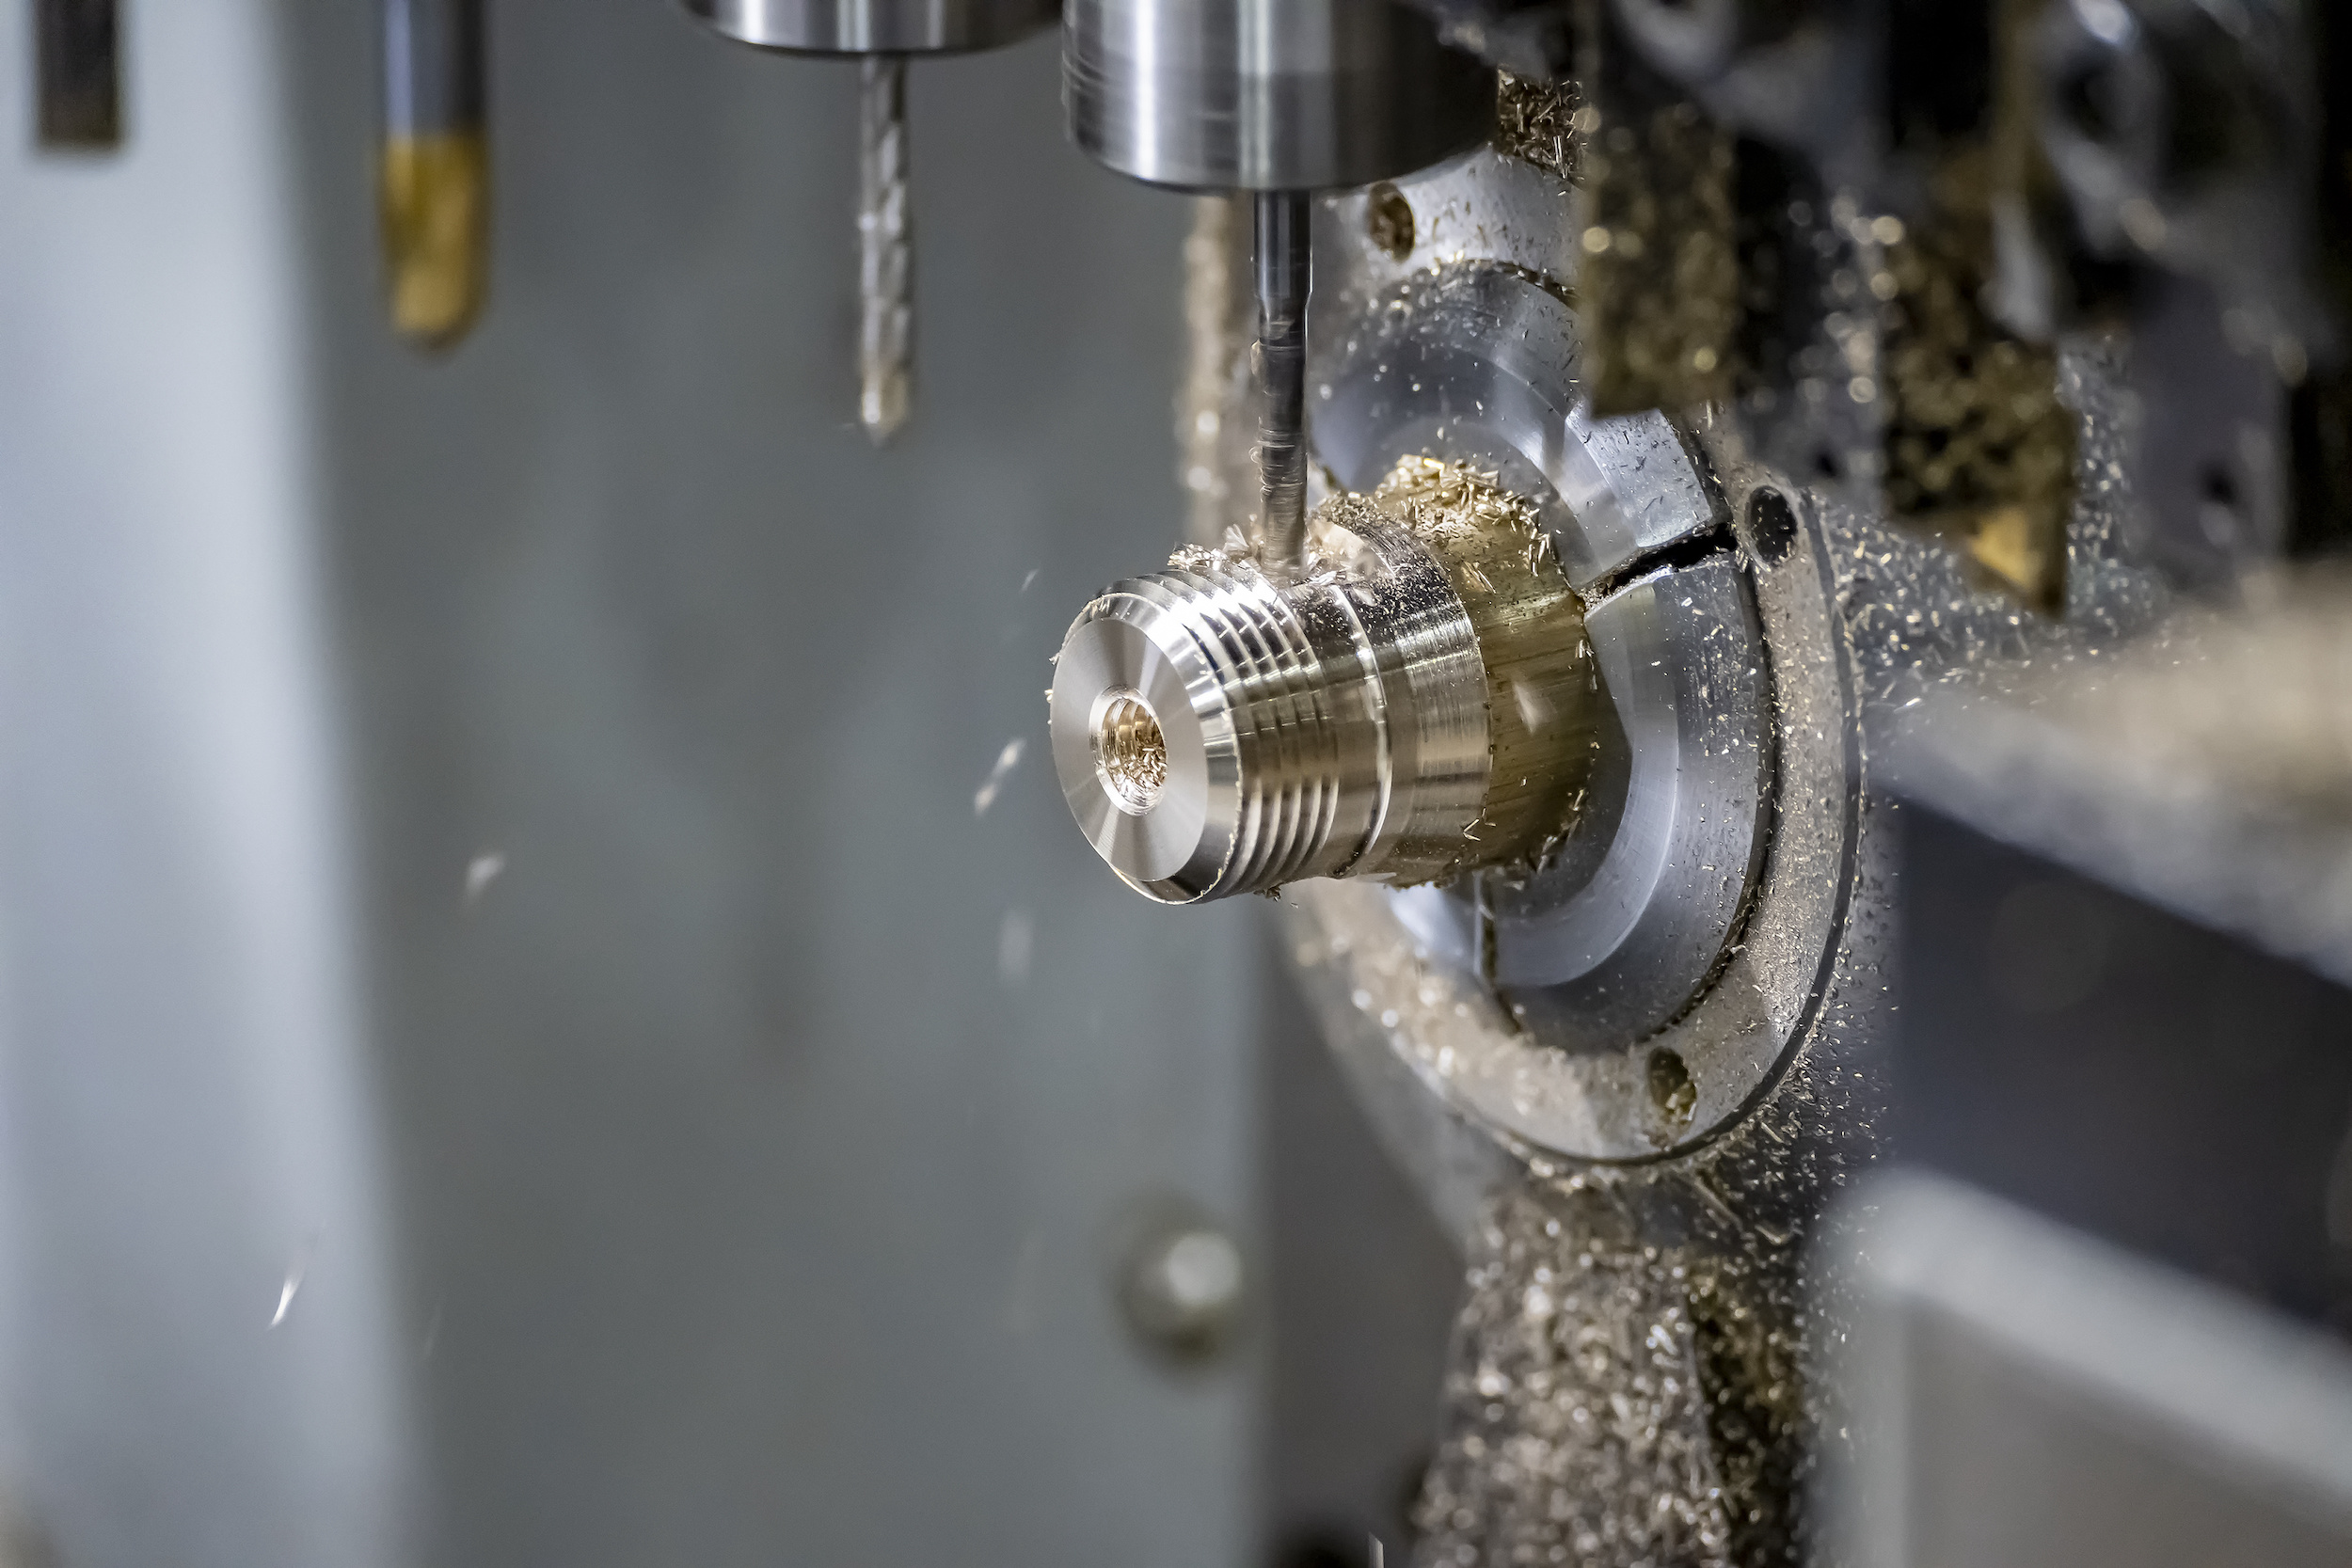
Because nitriding adds only a thin case with very little growth, parts can often be finished close to final size before they go out for processing. That is why our nitride services are popular for gears, spools, and tooling that cannot tolerate distortion.
Aluminum Nitride and Nitriding-Grade Steels
Aluminum plays a useful role in nitriding steels. Nitriding grades such as Nitralloy 135M contain aluminum, which forms very hard aluminum nitride precipitates in the diffusion zone and gives these steels their high surface hardness and strong case.
A note for buyers: aluminum nitride is also the name of a technical ceramic, and the nitriding process described on this page is not used to produce it or to harden aluminum parts. Our nitride services are for steel and other nitriding-grade alloys. If you need hardened surfaces on aluminum components, ask us about hard anodizing and other coatings instead.
Specifications
| Surface Hardness | Rc 60–72 compound layer; material dependent. 4140 and 4340 typically achieve Rc 62–65. |
| Case Depth | 0.005″ to 0.030″ total case depth; effective case depth of 0.010″ to 0.020″ is typical, per specification. |
| Processes | Ion nitriding (plasma nitriding) and gas nitriding; process selected according to part requirements. |
| Distortion | Minimal; typically less than 0.001″ dimensional change on properly machined parts. |
| Materials | 4140, 4340, H13, D2, 17-4 PH, Nitralloy 135M, and other nitriding-grade steels. |
| White Layer | Controllable thickness per specification; ion nitriding can eliminate the white layer upon request. |
| Specifications | AMS 2753 (plasma nitriding), AMS 2759/10, and customer-proprietary specifications. |
| Documentation | Hardness traverse, case depth reports, and white layer measurements provided with finished parts. |
| ISO | ISO 9001:2015; outside suppliers qualified under RPM’s approved vendor procedures. |
Applications for Nitrided Precision Parts
Nitriding is the preferred surface hardening method for precision components where dimensional accuracy must be maintained after hardening:
- Gears and gear shafts — hard tooth flanks with minimal distortion of gear geometry
- Cams and cam followers — wear-resistant surfaces on complex contour profiles
- Hydraulic and pneumatic spools and sleeves — hard bore surfaces for long service life
- Extrusion screws and barrel liners — extreme wear resistance in abrasive processing applications
- Tooling and fixtures — hard surfaces for repeated use without dimensional degradation
- Aerospace actuator components — fatigue life improvement combined with surface hardness
Frequently Asked Questions
What steels are suitable for nitriding?
Not all steels respond equally to nitriding. Steels containing nitride-forming alloying elements chromium, molybdenum, aluminum, and vanadium achieve the best nitriding response. Common nitriding steels include 4140, 4340, H13, D2, and dedicated nitriding grades such as Nitralloy 135M. Plain carbon steels (1018, 1045) can be nitrided but achieve lower hardness than alloy grades.
What dimensional change should I expect after nitriding?
Properly machined and stress-relieved parts experience less than 0.001″ dimensional change through nitriding. Parts with significant machining-induced stress or thin wall sections may experience slightly more growth. We recommend stress relieving before nitriding for precision components to minimize distortion.
Can nitriding be applied selectively to some surfaces but not others?
Yes. Surfaces that should not be nitride can be protected by masking with copper plating or mechanical stop-off. Threads, precision bores, and functional surfaces that must remain at base material hardness are commonly masked during the nitriding process.
Is the white layer a problem for my application?
The white layer is a very hard, brittle compound layer on the surface. For most wear applications it is beneficial. For applications requiring a highly polished surface, fatigue loading, or subsequent grinding, the white layer may need to be removed or minimized. Ion nitriding can produce very thin or near-zero white layer thickness per specification.