EDM Service
Resolute Precision Manufacturing (RPM) offers an EDM service covering both wire EDM and sinker EDM for precision machined components that need features conventional cutting tools cannot produce. Thin slots in hardened steel, precise internal profiles, small-radius corners, and features in exotic alloys are all within the scope of electrical discharge machining. We coordinate the process through qualified outside providers and deliver EDM-finished parts from a single purchase order. Request a QuoteWhat EDM Produces That Conventional Machining Cannot
Electrical discharge machining removes material with electrical sparks rather than cutting forces. That difference gives EDM a unique set of capabilities.
- It cuts any conductive material, whatever its hardness. Hardened D2 tool steel at Rc 60 machines as easily by EDM as soft aluminum. Conventional cutting tools deflect, chatter, and wear rapidly in hardened materials. EDM does not.
- It produces near-zero internal corner radii. Narrow slots, square inside corners, and contours with no minimum radius constraint are all possible.
- It puts no cutting force on the workpiece. Fragile thin walls and delicate sections can be EDM-machined without deflection or damage.
Wire EDM vs. Sinker EDM
Two EDM processes serve different geometric requirements.
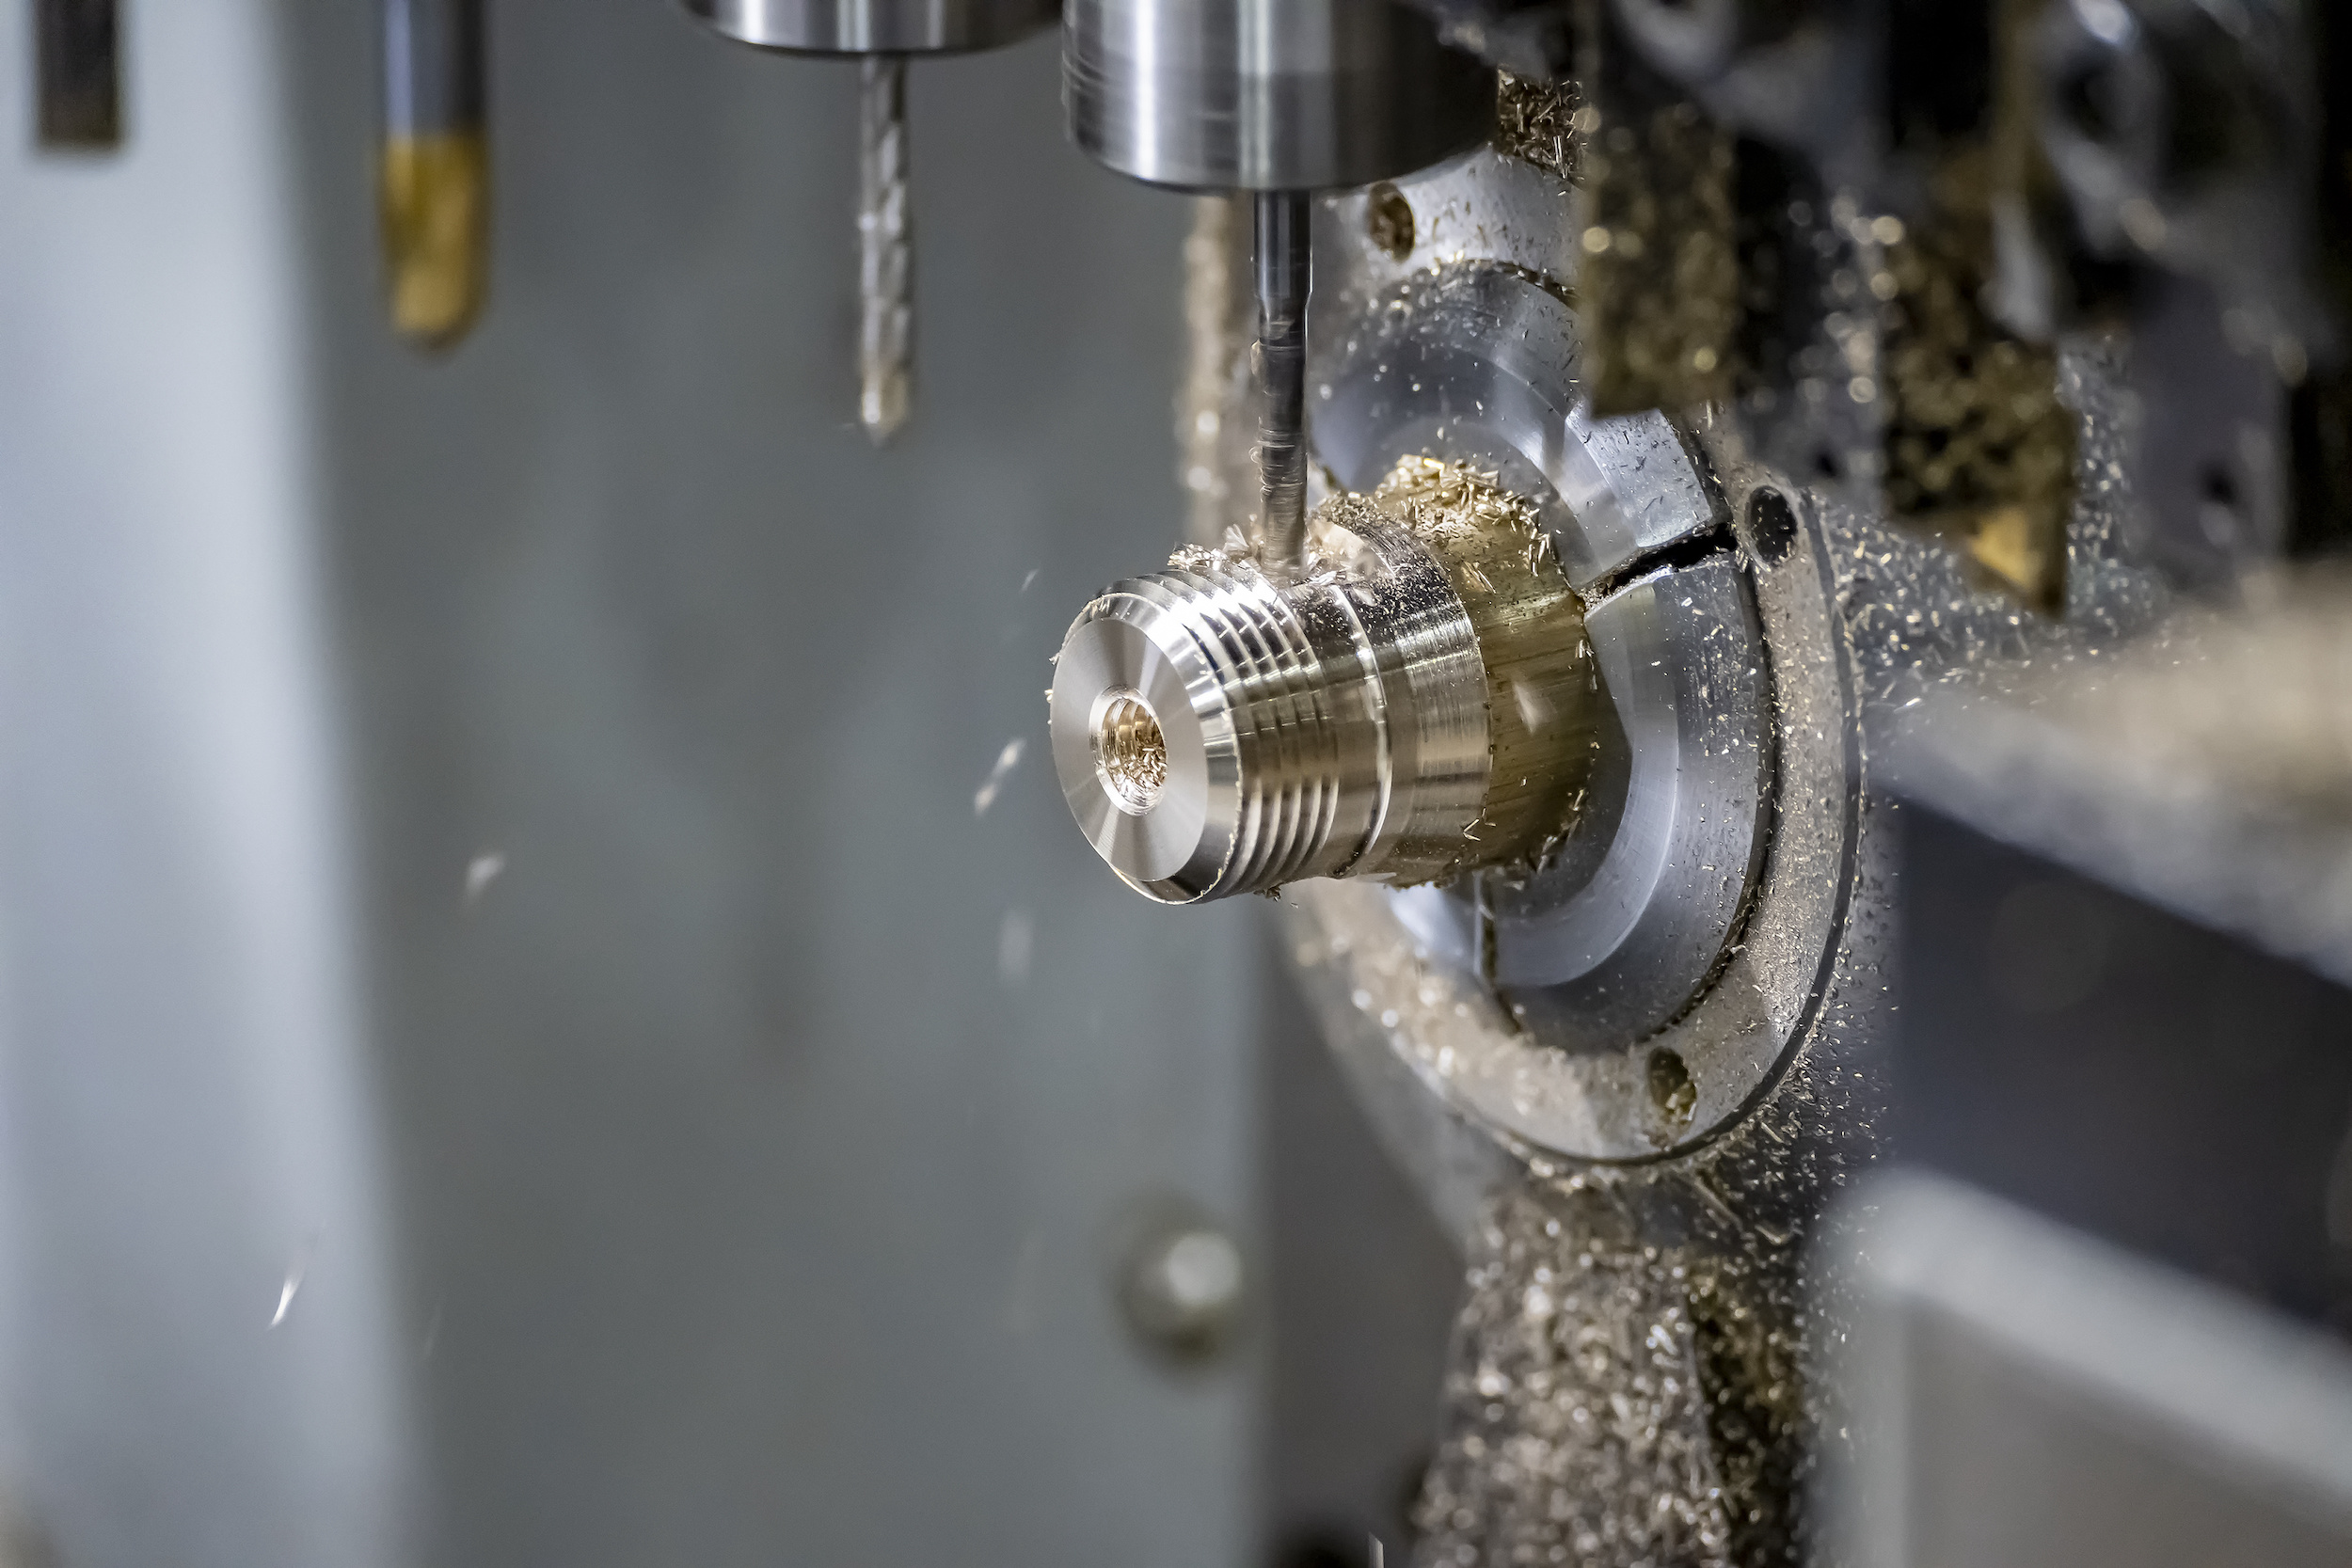
- Wire EDM: a thin brass wire (typically 0.004″ to 0.012″ in diameter) travels through the part, cutting a precise contour path programmed from your drawing. It is used for through-cuts such as gear profiles, extrusion dies, keyways in hardened parts, thin slots, and precise contour profiles.
- Sinker EDM (die sinker): an electrode machined to the shape of the desired cavity is fed into the workpiece, eroding the cavity shape. It is used for blind features such as injection mold cavities, blind slots, recesses, and internal profiles a wire cannot reach.
Precise EDM Services for Tight-Tolerance Parts
When a feature must hold tolerance after hardening, precise EDM services are often the only practical route. Wire EDM holds ±0.0002″ on contours, and our EDM service can finish profiles that would be impossible to cut with an end mill. Because the part is already at its final hardness, there is no distortion from post-hardening cutting and no tool wear to compensate for.
We use precise EDM services for parts such as:
Gear and spline profiles in hardened steel
Extrusion and stamping die components
Keyways and slots in heat-treated shafts
Thin-wall and fragile features in medical and aerospace parts
Carbide, titanium, and Inconel components
Sinker EDM Services for Blind Cavities and Complex Shapes
Our sinker EDM services use custom copper or graphite electrodes to produce cavities, slots, and recesses that wire cannot reach. The electrode is machined to the inverse of the finished feature, then fed into the workpiece to erode the shape. This makes sinker EDM services well suited to mold cavities, deep ribs, blind keyways, and sharp-cornered pockets in hardened tool steel.
Typical accuracy is ±0.0005″ on cavity features, and surface finish can be improved with finishing passes when the application needs it.
Specifications
| Wire EDM | Brass wire (0.004″–0.012″ diameter) for through-cut profiles in any electrically conductive material; taper cutting available. |
| Sinker EDM | Custom copper or graphite electrodes for blind cavities, slots, and recessed features. |
| Material | Any electrically conductive material, including hardened steel, carbide, titanium, Inconel, copper, and aluminum. |
| Dimensional Accuracy | Wire EDM: ±0.0002″ on contours; Sinker EDM: ±0.0005″ on cavity features. |
| Surface Finish | Ra 8–32 microinch as-cut; finer finishes available with additional skim passes. |
| Minimum Slot Width | 0.005″ minimum through-slot; dependent on material and part geometry. |
| Minimum Inside Radius | Approximately equal to the wire radius (0.002″–0.006″) for Wire EDM. |
| Documentation | Process certifications and dimensional inspection reports provided with finished parts. |
| ISO | ISO 9001:2015; outside suppliers qualified under RPM’s approved vendor procedures. |
When to Specify EDM on Your Drawing
Specify EDM when your part has one or more of these requirements:
Features in hardened or heat-treated material that must be produced after hardening
Narrow slots or keyways where the width is too small for a standard end mill
Internal corners with near-zero radius requirements
Thin-wall features where cutting forces would cause deflection or damage
Exotic alloy features where tool wear in conventional machining is prohibitive
High-accuracy contour profiles that require ±0.0002″ or better dimensional tolerance
Frequently Asked Questions
Can EDM machine parts that have already been hardened?
Yes this is one of EDM’s primary advantages. Wire and sinker EDM machine hardened materials as readily as soft materials. Common practice is to rough-machine before hardening and EDM the precision features after eliminating distortion risk from post-hardening conventional machining.
What is the surface finish produced by wire EDM?
Wire EDM typically produces Ra 16–32 microinch in the as-cut condition. Multiple skim passes improve surface finish to Ra 8 or better. For bearing surfaces and sealing faces, we specify additional skim passes or subsequent grinding to meet finish requirements.
Can wire EDM cut through thick sections?
Yes. Wire EDM cuts through any thickness of conductive material that fits within the machine’s Z-axis travel. Common cut heights range from a fraction of an inch to 12 inches or more. Taper angle capability allows cutting of die and punch profiles with draft angles.
What lead time should I expect for EDM operations?
Typical EDM turnaround through our outside supplier network is one to two weeks for standard wire EDM work. Complex sinker EDM with custom electrode fabrication may require two to three weeks. We schedule EDM operations in parallel with other outside operations where possible to minimize total elapsed time.