CMC Gun Parts
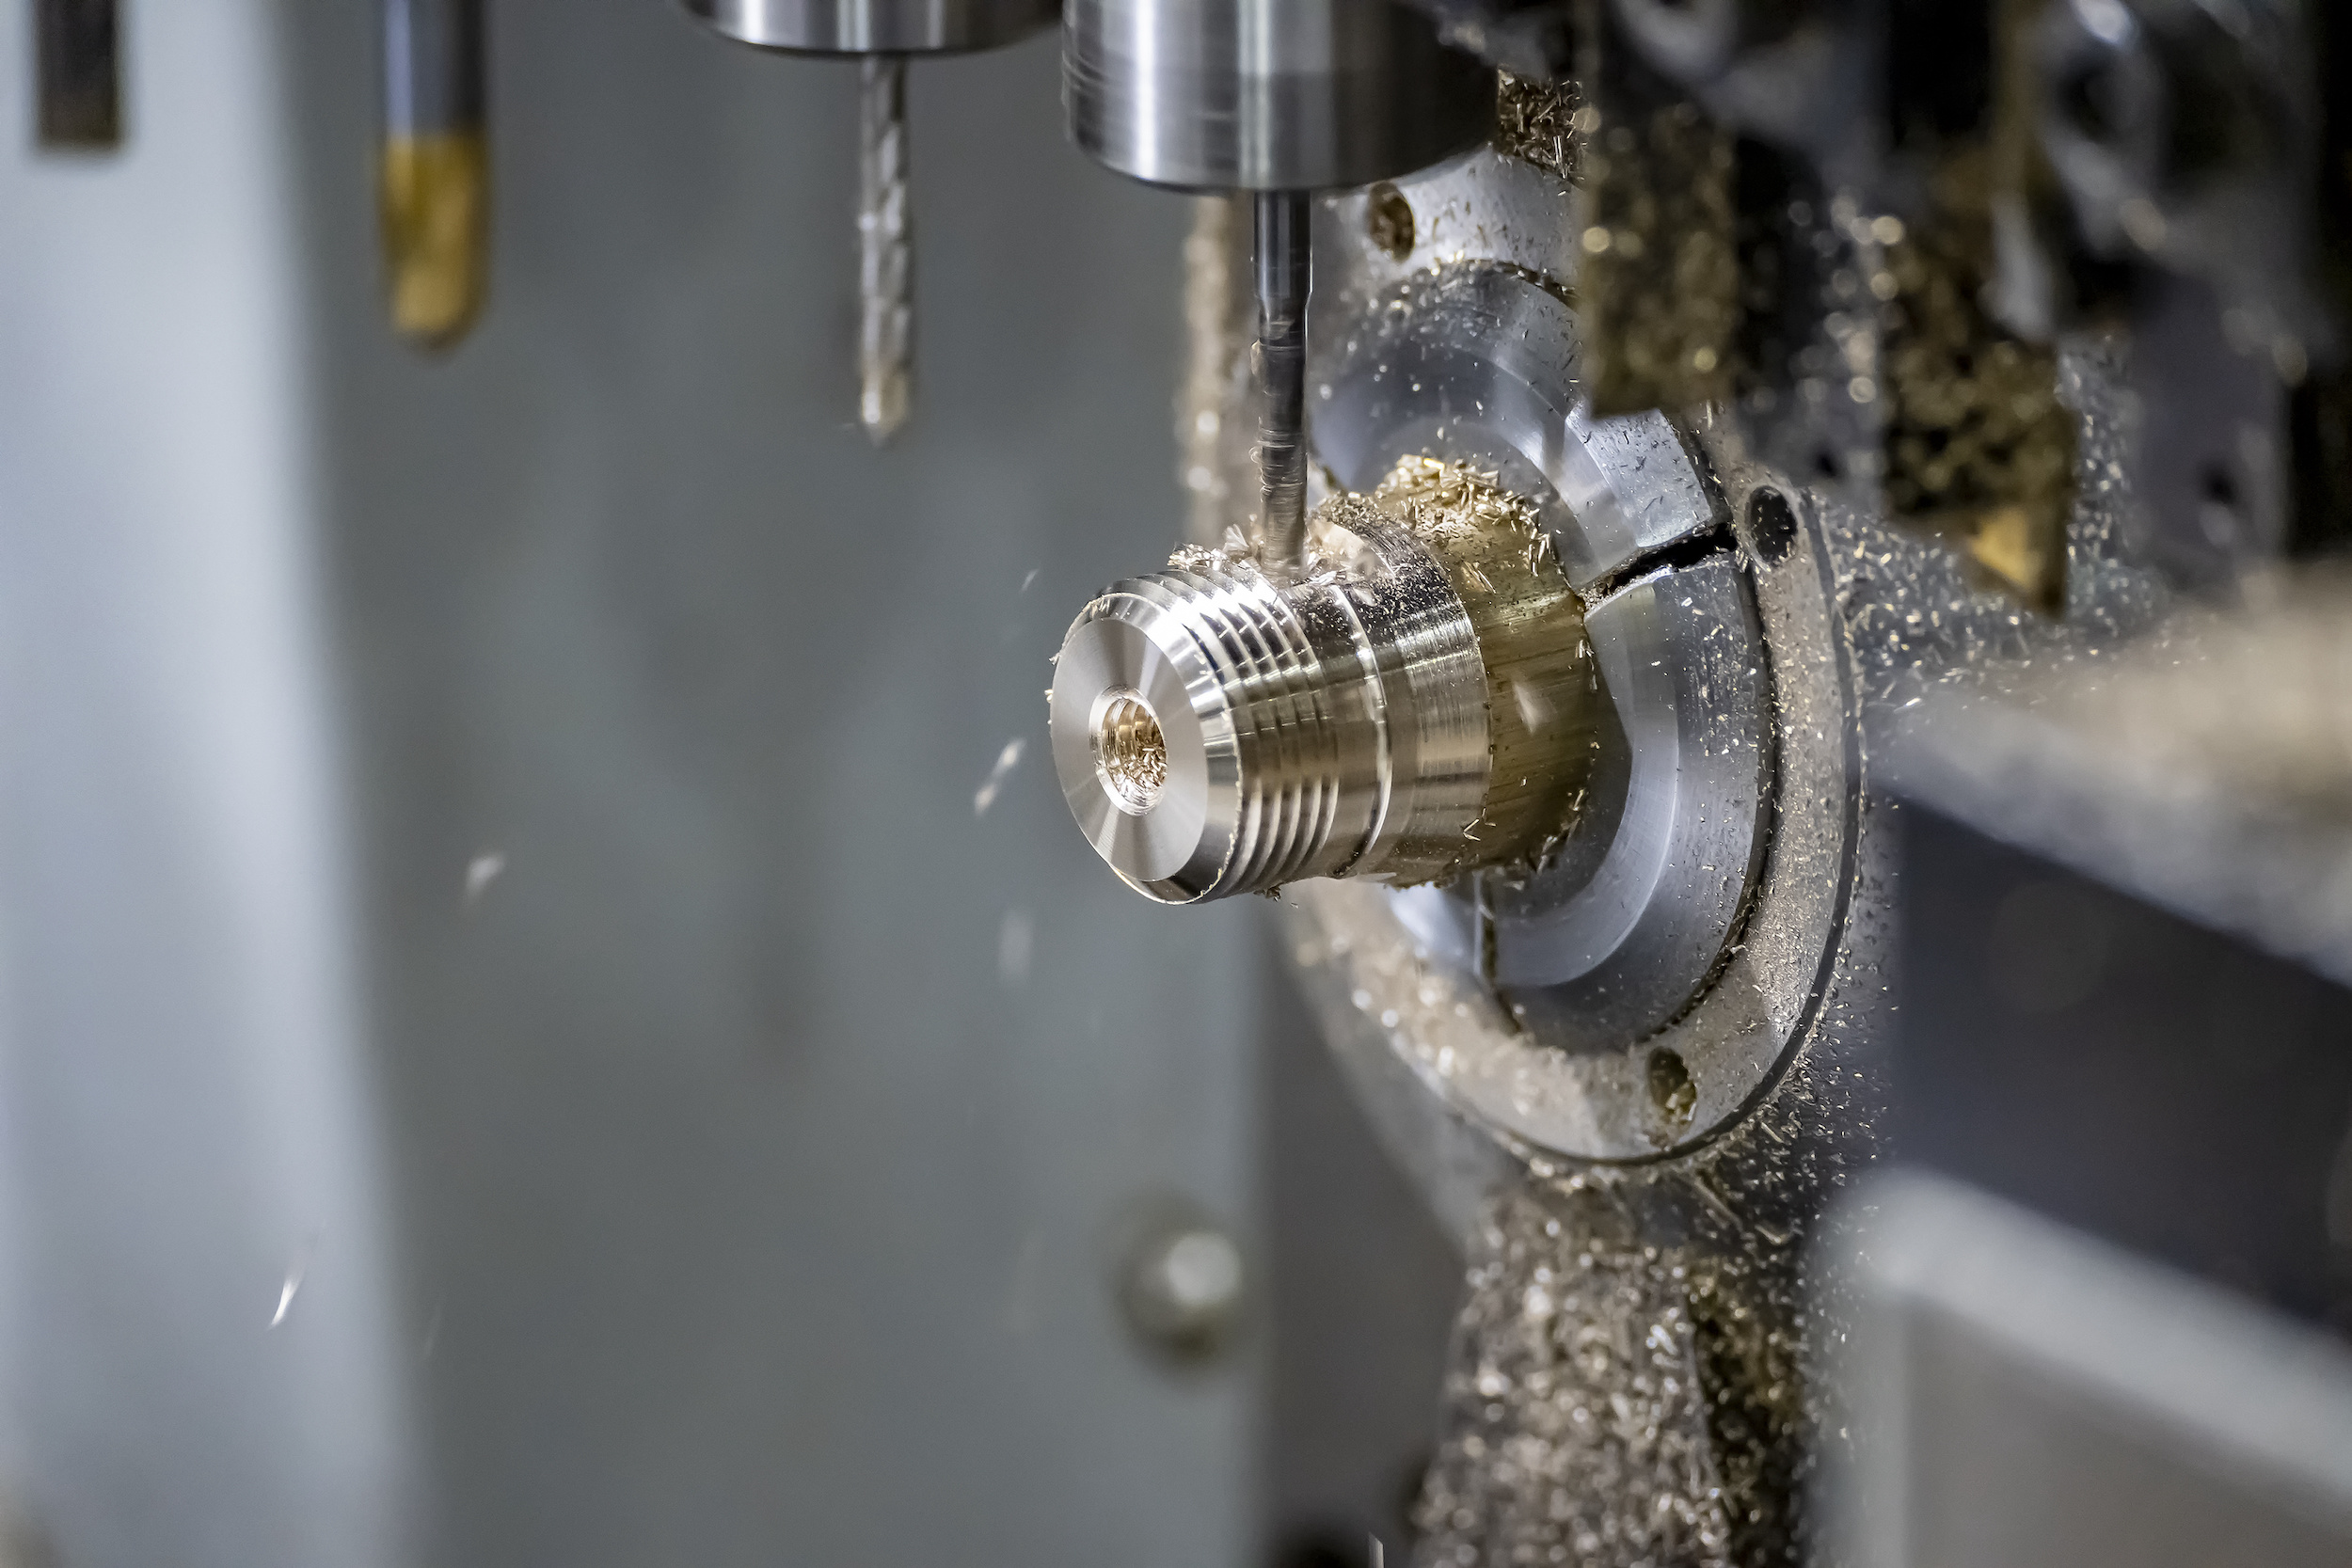
Resolute Precision Manufacturing produces custom machined components (CMC) for the firearms and shooting sports industry pins, small hardware, housings, and structural components machined to tight tolerance in aluminium, alloy steel, and stainless steel. RPM manufactures components to customer drawings and specifications; we do not design, assemble, or sell complete firearms. Our Swiss CNC and multi-axis milling equipment hold the dimensional consistency and repeatability that firearm component programs require, and our ISO 9001:2015 quality system provides the material traceability and documentation our customers need to support their own regulatory and quality obligations. Request a QuoteWhy Precision and Consistency Matter
Firearm components function as part of a mechanical system where fit, interchangeability, and repeatable dimensions directly affect reliability. A pin, detent, or housing that is out of tolerance on one production lot but not another creates downstream assembly and function problems for our customers. RPM’s CNC platforms are built around lot-to-lot repeatability: the same program, the same fixturing, and the same in-process inspection plan run on every production release, so part 1 and part 10,000 measure the same.
Our Services
Materials We Machine
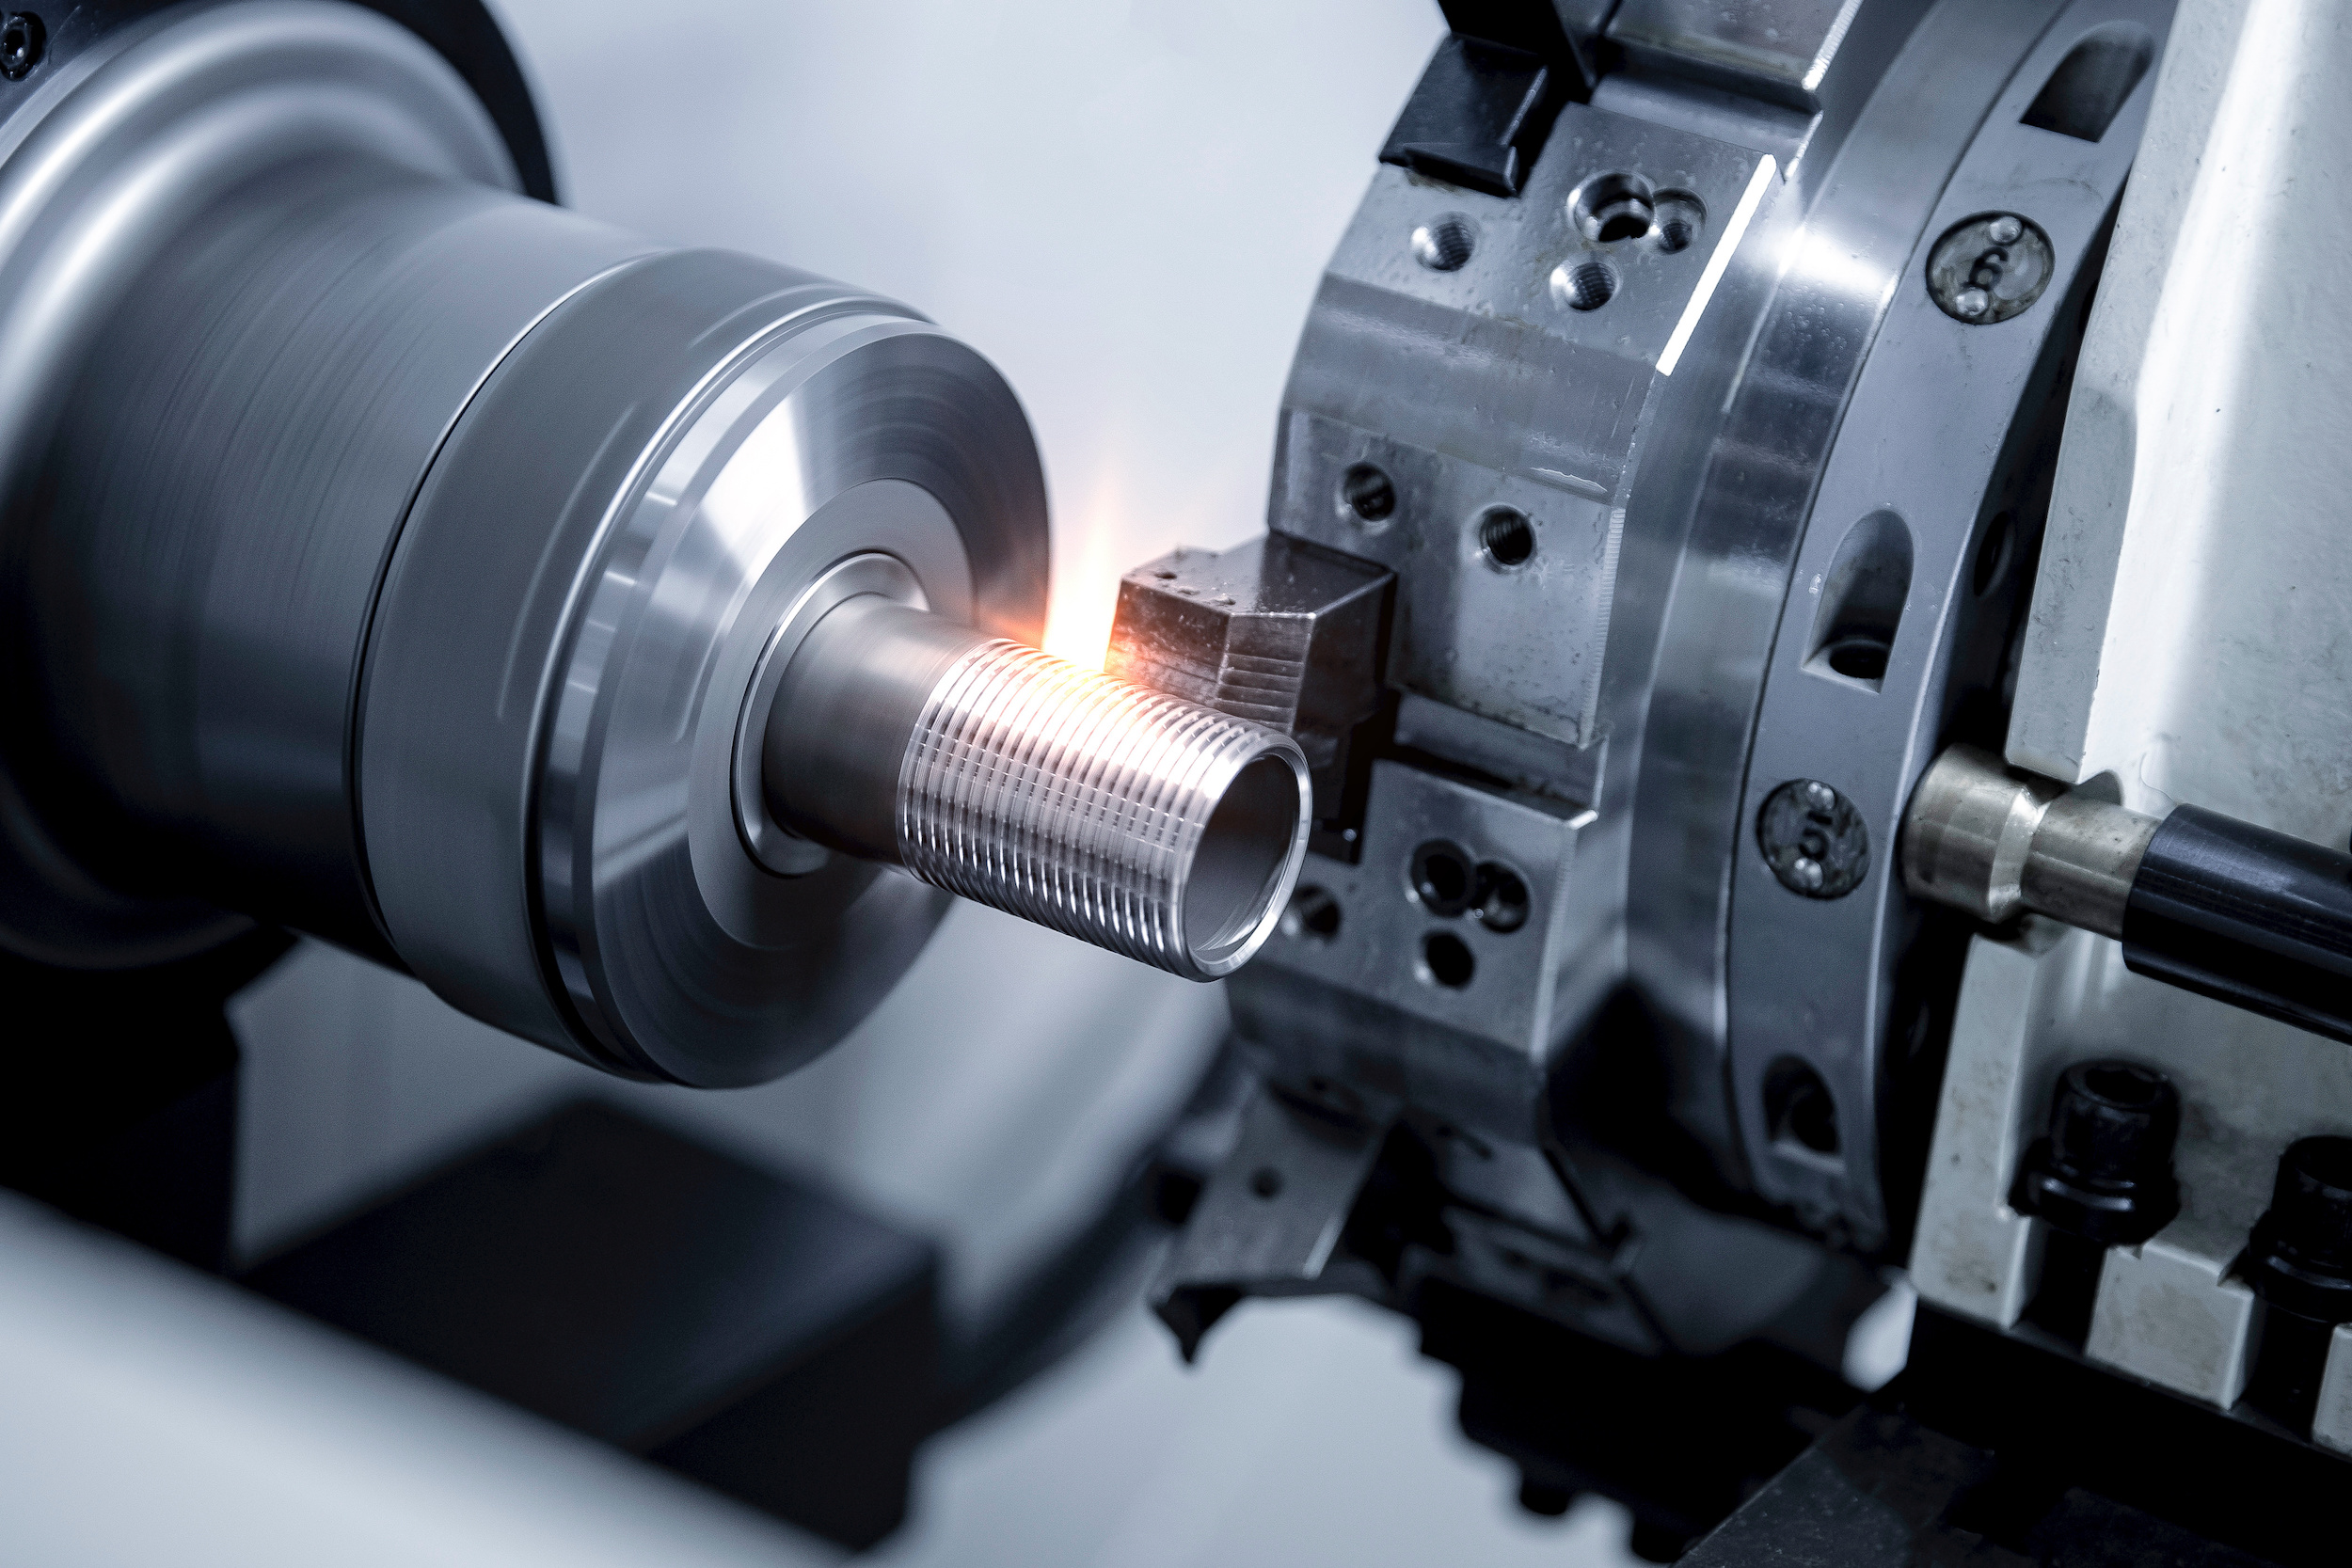
Our live tooling lathes complete all of the following shaft features without secondary operations:
- Aluminum 7075-T6 and 6061-T6 high strength-to-weight components, housings, and structural hardware
- Alloy steel 4140 and 4340 — pins, bushings, and hardware requiring heat treatment for wear resistance
- Stainless 416 and 17-4 PH — corrosion-resistant small parts, springs housings, and precision hardware
- Brass and bronze — low-friction bushings, detents, and wear components
Capabilities for Firearm Component Programs
- Swiss CNC turning for small-diameter pins, screws, and detent components with tight OD and length tolerances
- Multi-axis milling for housings, frames, and structural components requiring multiple features in one setup
- Coordinated outside operations heat treat, black oxide, nitride, and other coating processes for finished, ready-to-assemble parts
- Production runs from prototype quantities through established recurring-production volumes
Specifications
| Diameter Range | Small shafts on Swiss CNC (up to 38mm); standard shafts bar-fed up to 3.2″; large shafts chucked up to 25.5″ |
| Milling | 3, 4, 5-axis vertical milling for housings and structural components |
| Tolerances | Routinely ±0.001″; ±0.0005″ achievable on critical features |
| Outside Operations | Heat treat, black oxide, nitride, zinc plating — coordinated and certified |
| Quality | ISO 9001:2015; material traceability; first article inspection on request |
| Volume | Prototype through established production quantities |
| Scope | Components manufactured to customer drawing; RPM does not manufacture or assemble complete firearms |
Frequently Asked Questions
Does RPM manufacture complete firearms?
No. RPM manufactures individual machined components to customer drawings and specifications. We do not design, assemble, sell, or ship complete firearms.
Can RPM provide material traceability for firearm component programs?
Yes. Material traceability to certified mill heat numbers is standard, with certifications retained and referenced to specific production lots for the retention period your program requires.
Can RPM coordinate coatings such as black oxide or nitride for gun parts?
Yes. Through our value-added services network we coordinate heat treat, black oxide, nitride, and plating so parts arrive finished and ready to assemble.
What order volumes does RPM support for firearm components?
We quote prototype and low-volume development quantities as well as established recurring-production releases. Discuss your program’s volume with our team during quoting.