Most people who buy precision machined parts have never seen a machine shop floor. They send a drawing, receive a quote, approve a purchase order, and eventually receive a box of parts. What happens in between – the actual process of turning a drawing into a finished machined component – is invisible.
This article walks through every step of how a custom machined part goes from your drawing to your dock. Understanding the process makes you a better customer: you will specify drawings more effectively, set realistic expectations for lead time, and understand why certain features cost more than others.
Step 1: Drawing Review and Manufacturing Feasibility
Before a machine shop quotes a part, an engineer reviews the drawing. This is not a formality – it is a genuine engineering assessment of whether the part can be manufactured as drawn, and at what cost.
During drawing review, the engineer is looking for:
- Process selection – which machines will run this part (turning, milling, Swiss, mill/turn)?
- Tolerance feasibility – can every toleranced feature on the drawing be held by the identified process? Are any tolerances tighter than the process can consistently deliver?
- Material selection – is the specified material available in bar or billet form? Are there better alternatives?
- Feature geometry – are there features that require special tooling, that are difficult to access, or that would be better achieved by a different design?
- Quantity economics – at the quoted volume, which setup strategy minimizes cost per part?
A direct machine shop – one where you are talking to the engineers and machinists who will actually run your job – will tell you at this stage if there are problems with the drawing that will affect cost or quality. That is the value of the feasibility note: it is a technical conversation before money changes hands.
Pro Tip
Include your functional intent with the drawing when you request a quote. ‘This shaft must achieve ±0.0005″ concentricity between bearing seats because it runs in a sealed angular contact pair at 10,000 RPM’ tells the machinist far more than the tolerance callout alone. It allows them to advise on the right process, the right sequence, and any design changes that would reduce cost without compromising function.
Step 2: Quoting and Order Entry
Once the drawing review is complete, the shop generates a quote based on the identified process, setup strategy, cycle time estimate, material cost, and overhead. At a direct machine shop, this quote reflects actual machining costs – not a distributor’s margin added on top.
When you approve the quote and issue a purchase order, the order enters the production system. The traveler – a document that accompanies the part through every step of production – is generated. The traveler contains the part number, revision, quantity, material specification, operations sequence, inspection requirements, and any special instructions from your drawing or purchase order.
Step 3: Material Procurement
For most standard materials – 1018 steel, 6061 aluminum, 303 stainless, 360 brass – a machine shop maintains bar stock inventory in common sizes. Your order pulls from stock and production can begin immediately.
For specialty materials – 17-4 PH stainless, Grade 5 titanium, Inconel 718, PEEK – material must be procured from a supplier. This is the primary driver of lead time for specialty material parts: the material procurement cycle, not the machining cycle.
Material is received with a mill certification – a document from the material manufacturer confirming the alloy, heat number, and chemical composition. The heat number is recorded on the traveler and retained for traceability. If you ever need to trace a production part back to a specific heat of material, the heat number record makes that possible.
Step 4: Setup
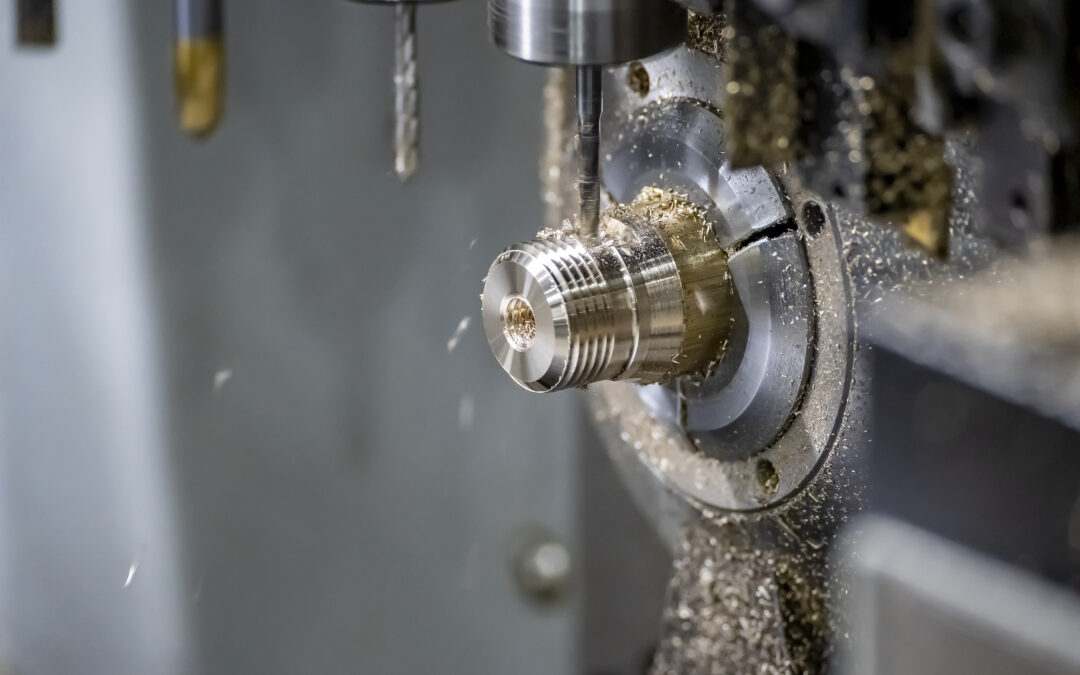
Setup is the process of preparing the machine to run a specific part. For a CNC turning job, setup includes loading a bar of the correct material into the bar feeder, installing the correct tooling in the turret (OD turning inserts, boring bars, threading tools, live tooling), writing or loading the part program, and dialing in the dimensions with test cuts on the first piece.
Setup time is a real cost — typically one to four hours for a standard turned part, longer for complex mill/turn parts. This cost is fixed regardless of quantity: a 10-piece prototype and a 10,000-piece production run both require the same setup. At low quantities, setup cost dominates per-part cost. At high quantities, setup cost is amortized across many parts and becomes a small fraction of the total.
Step 5: First Article Inspection
Before production quantity begins, the first completed part is fully inspected against the drawing – every dimension, every tolerance, every callout. This is called the first article inspection (FAI).
The purpose of first article inspection is to confirm that the setup – tooling, program, offsets – produces a part that meets drawing requirements. If any dimension is out of tolerance on the first article, the setup is adjusted and another first article is run before production begins.
No reputable machine shop runs production quantity before the first article is approved. Skipping first article inspection to save time is how machine shops ship hundreds of non-conforming parts to customers.
Step 6: Production
Once the first article is approved, production runs. On a bar-fed turning cell, the machine runs largely unattended — bar stock feeds automatically, parts complete and drop into the catch bin, and the machine advances to the next bar length. The operator monitors the machine, checks parts at defined intervals per the production control plan, and changes tooling as required by the tool life program.
In-process inspection happens at defined intervals during production. Critical dimensions are measured — not just visually inspected — and recorded on the traveler. If a dimension drifts toward the tolerance boundary, the operator makes a tool offset adjustment before the dimension goes out of tolerance. This is statistical process control (SPC) in practice: catching variation before it becomes scrap.
Step 7: Outside Operations (If Required)
Many parts require operations that the machine shop does not perform in-house: heat treating, grinding, EDM, anodizing, zinc plating, passivation. These outside operations happen between machining and final inspection.
At Resolute Precision, we manage outside operations for you. We ship to our qualified outside processors, receive the parts back, and perform incoming inspection before they proceed to final inspection and shipment. You do not coordinate with four different suppliers – you deal with one, and we handle the rest.
Step 8: Final Inspection
After machining and any outside operations, final inspection verifies that the finished parts meet drawing requirements. Critical dimensions are measured and recorded. Cosmetic requirements – surface finish, edge condition, marking – are verified. Quantity is confirmed.
Parts that fail final inspection are either reworked to drawing (if the non-conformance is correctable), scrapped (if it is not), or submitted for customer disposition (if the non-conformance is minor and may be acceptable). A certificate of conformance – signed by an authorized quality representative – certifies that the shipped parts meet drawing and purchase order requirements.
Step 9: Packaging and Shipment
Finished parts are packaged to protect machined surfaces during transit. Precision turned parts are typically layered in tissue paper or poly bags to prevent surface-to-surface contact and scratch damage. Particularly delicate surfaces – lapped faces, ground ODs, polished bores – receive additional protective wrapping.
The traveler accompanies the shipment, and the certificate of conformance, material certifications, and any required process certifications are included in the delivery documentation.
How Long Does All of This Take?
Lead time – the elapsed time from purchase order to delivery – depends on material availability, current shop capacity, and part complexity. For standard materials in stock, a typical precision turned part runs one to three weeks from order to shipment. For specialty materials requiring procurement, add one to two weeks for material lead time.
The fastest way to reduce lead time is to establish a blanket order program – an annual purchase order with scheduled release quantities. With a blanket order, material is pre-stocked, setups are maintained, and releases ship within days rather than weeks.
Summary
Custom machined parts start as a drawing and end as precisely dimensioned components on your dock – but the journey involves engineering review, material procurement, machine setup, first article approval, production with in-process control, outside operations, final inspection, and documented shipment. Understanding each step helps you write better drawings, set realistic expectations, and ask better questions when you evaluate machine shop partners.
At Resolute Precision, you deal directly with the people who run every one of these steps. When you call, you reach the engineers and machinists who reviewed your drawing, set up your job, and ran your parts. That is the direct manufacturer difference.
Have a Part to Quote?
Send us a drawing. We will have a manufacturing feasibility note and real price back to you within 24 hours. No commitment, no pressure – just a straight answer from the people who will run your job. Contact Us or call (260) 665-6463.